Welding is a set of decisions made in a fixed order: which process the metal and the joint allow, how thick the section is, whether the part can be moved to a bench or has to be welded where it sits, and only then what you set the machine to. Get the order wrong and no amount of fiddling with amperage saves the joint. Get it right and most of the remaining work is preparation and cleanliness.
Choosing the process before touching a dial
If the joint needs to be visually perfect, leak-tight, or made on thin material without distortion, the answer is TIG — gas tungsten arc welding, GTAW. It uses a nonconsumable tungsten electrode and an inert shielding gas, typically argon, to protect the molten pool from the atmosphere, and it is the process chosen for precise, high-quality welds on steel, stainless steel, and aluminum. If the job is structural, dirty, thick, or outdoors in wind, MIG or stick will finish it faster and cheaper, and the cosmetic penalty usually doesn't matter.
The reason TIG holds that position is control. The filler is added by hand, independently of the heat, so you can weld a joint with no filler at all, feather the amperage down at the crater, and watch the puddle rather than a shower of spatter. The cost is speed. TIG is slow, the operator needs both hands plus a foot or a fingertip on the current control, and the parts have to be clean — genuinely clean, wiped and wire-brushed to bare metal, because TIG has no flux and no slag to absorb what you left behind. Stick welding tolerates rust, mill scale, and paint at the joint edge. TIG does not. If someone is choosing their first process to learn on carbon steel, stick or MIG gets them laying bead sooner; TIG rewards patience with a steeper curve.
The limits matter too. TIG is poor outdoors in any breeze because the shielding gas is a soft column that wind strips away, and it's poor on very thick sections because the deposition rate is low. Aluminum is where it earns its reputation — alternating current gives the cleaning action that breaks up the oxide layer — but aluminum also demands more of everything: more heat, more gas, more attention to fit-up.
Gas, flow, and the parts of TIG that quietly ruin welds
Set argon flow for TIG in the range of 10–35 cubic feet per hour, and treat the middle of that band as the working zone rather than the top. On a specific power source — the LNT 25 — the recommended argon range is 10–15 liters per minute, which is a useful reminder that published flow figures come in different units and you should match the number to your machine's manual and your flowmeter's scale, not to a forum post. Too little flow and the pool is unprotected; too much and the gas column turns turbulent, aspirates room air at the edge of the cup, and you get porosity that looks exactly like too little flow. The symptom is the same, the fix is opposite, and the way you tell them apart is by watching the puddle and the cup rather than guessing.
The gas itself is usually pure argon, supplied as welding-grade at roughly 99.99% purity or higher. That purity is not marketing — a contaminated cylinder gives an unstable arc and dirty welds that you will chase for an hour before suspecting the gas. Argon-helium mixes come out for thicker aluminum and for stainless where you want more heat input into the joint without cranking amperage, and they cost more per cylinder and change the arc character enough that you should not switch mid-project without test beads.
Arc starting is the other place TIG quietly goes wrong, especially around electronics. High-frequency start is convenient but radiates interference; lift TIG starts the arc by touching the tungsten to the workpiece at low open-circuit voltage and then lifting it, which reduces the risk of high-frequency electromagnetic interference with nearby electronics. If you're welding near a control cabinet, a CNC, or a computer, lift start is the wrong feature to skip. The trade-off is that lift start marks the tungsten with a tiny bit of the base metal each time, so you dress the tip more often, and on aluminum the touch can contaminate the electrode badly enough to require a regrind.
Consumables and preparation eat more time than the welding does. Tungsten grind direction matters — grind lengthwise, not across the wheel, so the arc doesn't wander. Filler diameter should roughly match the joint thickness, and if you find yourself feeding rod faster than you can watch the puddle, the rod is too thin. Fittings, cups, and lenses are cheap; the habit of checking the cup for spatter before every pass is what keeps a $4 part from costing you a $400 weld.
Amperage, thickness, and the settings that follow from them
Set current from the material and thickness first, then adjust travel speed and gas to match; doing it the other way around produces a weld that looks acceptable and fails a bend test. Thin sheet wants low current and fast travel, thick plate wants high current and, on TIG, a bevel and multiple passes. Steel and stainless give you a visible puddle that tells you when to move; aluminum gives you a puddle that changes color and then suddenly sags, which is why aluminum TIG is a timing skill more than a heat skill.
Joint design is a decision people skip because it feels like fabrication rather than welding. A square butt on thin material is fine; anything thicker wants a bevel, a root gap, and a backing purge on stainless so the backside of the weld doesn't oxidize into sugar. Fit-up tolerance is where the process choice comes back to bite you: TIG will not bridge a sloppy gap the way stick will, and forcing it means either a cold, lumpy weld or a hole. Spend the time on the fit-up and the welding gets easy.
Distortion follows from heat input, and heat input follows from the order you weld in. Backstep, stagger, and clamp — in roughly that order of usefulness — and accept that a long seam will move no matter what. On stainless, the color of the heat tint tells you how much heat the metal saw, and if the customer cares about appearance after pickling, the tint you leave determines how much finishing they pay for.
Cutting: where the process dictates the machine
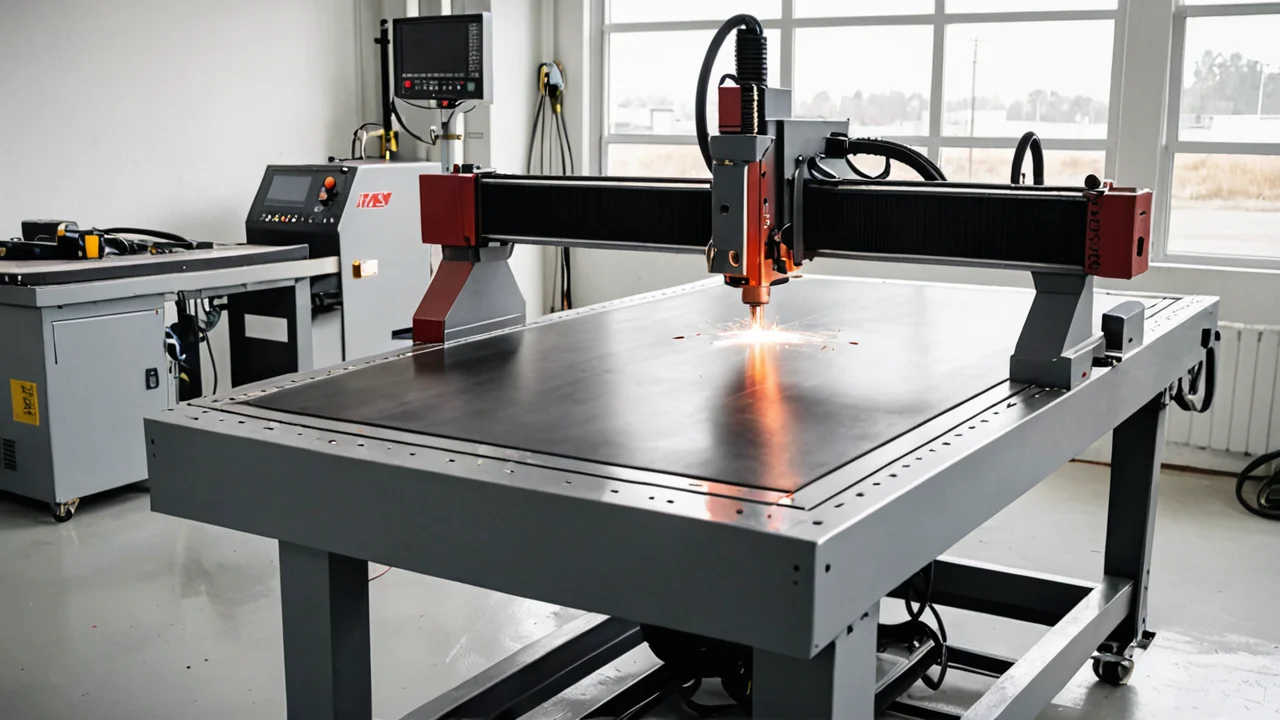
Plasma cutting needs a DC supply in the range of 200–400 volts DC to start and maintain the arc, which is why plasma cutters are not casual purchases — the power requirement, not the torch, drives the install. A 40 A air plasma cutter wants compressed air at 80–120 PSI and draws roughly 5.3 cubic feet per minute at that pressure. Under-supply the air and the cut quality collapses before the machine complains; the usual symptom is dross on the bottom edge and a kerf that widens toward the end of the cut. A small shop compressor that cycles constantly will deliver the pressure but not the volume, and the difference shows up as a good first inch and a ragged last foot.
Air plasma leaves a nitrided edge on the cut face and a heat-affected zone that has to be ground back before welding on it. That's the honest cost: plasma is fast and cuts any conductive metal, but the cut edge is not a weld-prep surface. For stainless and aluminum where the edge will be welded, a mechanical cut or a water table with the right gas mix is the better answer, and the plasma is for the rough-out.
For anything thin and straight, a shear or a saw beats plasma on both edge quality and cost per cut. Plasma wins on shapes, on thicker plate, and on material that can't be machined easily — and that's most of what a fabricator actually cuts.
What to buy first, and what to defer
Buy the machine that matches the material you actually weld, not the one that covers every case badly. A TIG machine with high-frequency and lift start, a decent foot pedal, and a quality torch covers steel, stainless, and aluminum up to the thickness a foot pedal can control; if the work is structural carbon steel, a MIG set with a gas bottle and a solid wire setup will out-earn the TIG for years. Stick is the cheapest entry into thick steel and the most tolerant of bad conditions — the machine costs little, the consumables cost little, and the process forgives a lot.
The order of spending that pays back fastest is: good helmet, good gloves, then the machine, then the extras. An auto-darkening helmet lets you see the joint before the arc starts, and a fixed-shade helmet teaches bad habits about head position that take a long time to unlearn. The gloves matter because TIG heat reaches the back of the hand through the glove faster than people expect on aluminum.
Defer the welder-positioner, the water cooler, and the spool gun until the work demands them. A water-cooled torch matters for production TIG at high amperage and for long beads; for hobby work an air-cooled torch is fine and one less thing to maintain. A spool gun for aluminum MIG is a specialist tool — if you're doing occasional aluminum, TIG covers it and the spool gun sits in the drawer.
The wrong purchase is the machine bought for the one job that needed it. If a project needs a 200 A machine once, rent or farm it out and spend the money on the process you'll use weekly.
Safety and the failures that show up later
Ventilation is the safety decision that most home welders get wrong, and it's the one that doesn't announce itself. TIG on clean steel produces little fume, which makes people complacent; welding on galvanized, painted, or oily metal produces zinc and hydrocarbon breakdown products that will make you sick the next morning and won't be obvious at the time. Weld outdoors or with extraction, and if you're welding anything coated, grind the coating back well past the weld zone first. Stainless fume is worse than carbon steel fume and the visible plume is not a reliable indicator of what you're breathing.
Arc flash and UV burns are the other delayed failure. The burn on your forearm shows up hours after you finish, which is why long sleeves and a leather bib are not optional even on a quick tack. Anyone within sight of the arc needs protection too — a bystander watching for a minute gets the same eye exposure you do.
The welding failures that show up later are mostly the ones that looked fine: lack of fusion at the root, porosity you couldn't see until the part was machined, and cracks that open because the joint was too restrained to move as it cooled. The way to catch them is to test — a bend test on a coupon, a dye penetrant check, a leak test — before the part goes into service. The cost of a coupon is trivial and the cost of a failed part is not.
The honest summary is that welding rewards the boring decisions. The process chosen for the material, the joint fit before the arc starts, the gas set in the middle of its range, the tungsten dressed and the metal clean, and the test run before the real part. The machine is the least interesting variable, and most of the problems people blame on the machine are one of the others.
Tungsten, cup size, and the gas coverage they actually produce
Gas flow and cup size are one decision, not two. A large cup on a ceramic lens lets you run a lower flow rate with coverage that reaches farther from the tungsten, which matters on titanium, on stainless where you're chasing a clean color, and on any joint with a deep groove. A small cup at the top of the flow range gives you a fast, narrow column that a draft will peel apart. If you push flow up to compensate for a cup that's too small for the joint, you're buying turbulence, not protection — the aspirated room air shows up as porosity and you'll blame the cylinder.
The tungsten size follows the current and the cup follows the joint. Too large a tungsten in a small cup and the arc starts off-center; too small a tungsten at high current and it balls, splits, or spits inclusions into the pool. On a machine like the LNT 25, where the argon recommendation is 10–15 L/min, the number assumes a cup and tungsten matched to the work — it is not a target to hit with any torch setup.
Post-flow, pre-flow, and the seconds nobody sets
Post-flow is the setting that protects the crater you just finished and the tungsten you just stopped. Cut the gas the instant the arc breaks and the pool, still molten, sees room air; the tungsten goes from shiny to colored and the next start is rough. Longer post-flow on stainless and on aluminum, shorter on thin steel where the pool freezes almost immediately. Pre-flow matters less on scratch and lift start and more on high-frequency start, where a short gas lead before the arc keeps the first instant of the puddle clean.
The trade-off is argon. Long post-flow on every tack empties a cylinder faster than the welding does, and on a job with hundreds of tacks that cost is real. Set it long enough to protect the stop, not long enough to feel generous.