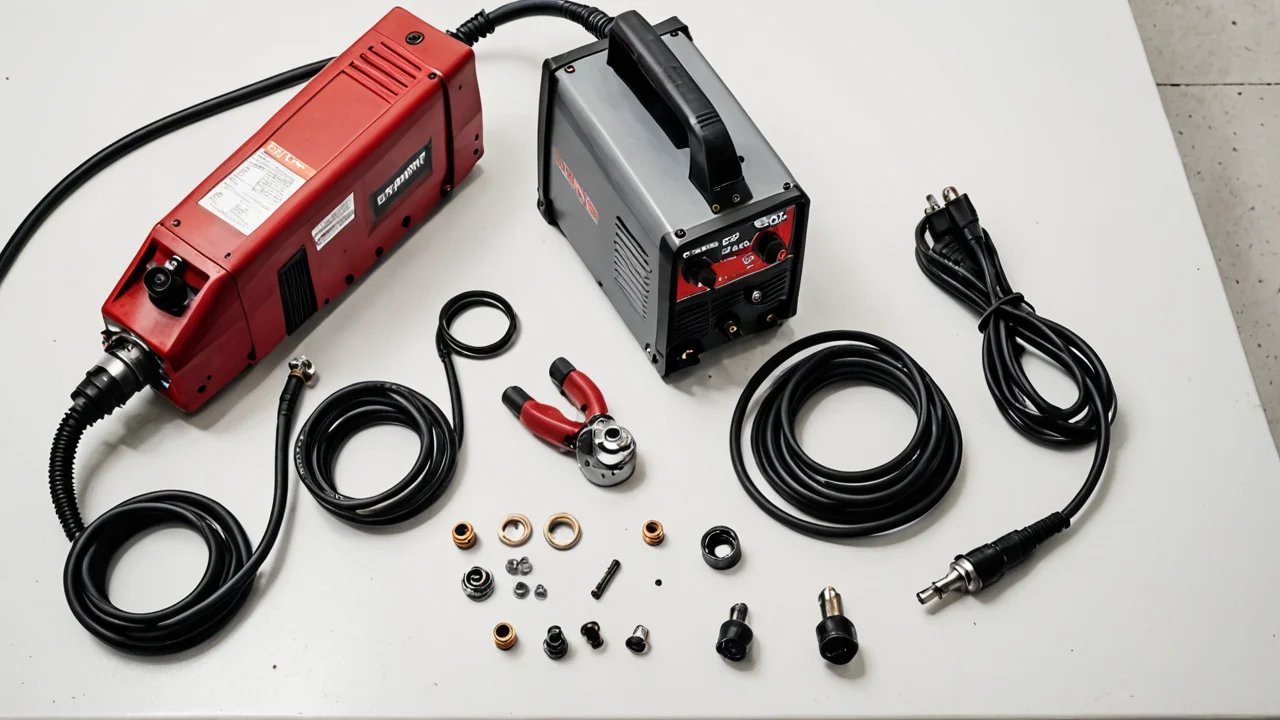
"Does a plasma cutter cut aluminum?"—this is the question every shop owner asks, and the answer is complex because it depends entirely on the specific setup and current draw. In short, yes, plasma cutters are engineered to process aluminum, but you must understand that plasma cutting works by forcing an extremely high-velocity, superheated stream of gas through a constricted orifice; this intense energy stream melts and expels the material, creating a clean cut path. The core mechanism involves establishing a voltage range of 200–400 volts DC to start and maintain this arc, which then uses extreme heat to reach cutting temperatures far exceeding standard oxy-fuel processes.
Selecting a Plasma Cutter Requires Balancing Power Requirements Against Specific Material Thicknesses
The most significant mistake new buyers make is assuming that simply having a high amperage rating (like 40 A) guarantees versatility; true value is found in matching the machine’s power output to the thickness and type of material you cut most frequently. Plasma cutters are rated by their cutting capacity, which dictates both the required input voltage and the necessary compressed air supply pressure. For instance, a common DC voltage range needed for operation is 200–400 volts DC. When sizing a machine, always consider the worst-case scenario thickness you need to cut in your shop, rather than focusing only on the thickest piece you might ever cut. The value proposition here isn't buying the largest cutter; it's finding the smallest cutter that meets your operational minimum specifications reliably.
The mechanical requirements for these machines are precise and non-negotiable. For a typical 40 A air plasma cutter, you need to maintain a compressed air supply pressure within the range of 80–120 pounds per square inch (PSI). This pressure is necessary because it directly drives the required airflow rate, which must be consistently around 5.3 cubic feet per minute (cfm) at that specified pressure. If your shop’s existing compressor cannot maintain this minimum PSI, no matter how expensive the cutter head is, it will underperform or fail to start an arc reliably.
However, looking only at amperage and air supply can be misleading because you must also factor in duty cycle—how long the machine can run at full power before overheating. A cheaper unit might advertise high peak amps but suffer from a very poor duty cycle, meaning it will overheat and shut down during a prolonged job. This operational limitation often costs more time (and labor) than the initial savings on the equipment.
Gas Shielding vs. Air Cutting Determines Your Operational Environment
When evaluating value, you must first decide if your work requires gas-assisted cutting or standard air plasma cutting, as this choice dictates fundamental machine components and operational costs. Standard plasma cutters rely on forced compressed air to facilitate the cut itself, providing high speed across most metals.
However, for specialized processes like TIG welding (Gas Tungsten Arc Welding, GTAW), which is used for precise, high‑quality welds on materials such as steel, stainless steel, and aluminum, you are dealing with a different value consideration entirely: the shielding gas. In TIG welding, pure argon—which should be supplied at high-purity welding‑grade argon (around 99.99% or higher)—is critical because it forms a protective barrier around the molten weld pool. This inert gas prevents contamination from oxygen, nitrogen, and water vapor in the air, which otherwise causes defects like porosity. If you are doing both plasma cutting and TIG welding, ensure your setup can handle multiple gas lines safely.
For TIG itself, the required shielding gas flow rate is highly dependent on the power source; for example, using an LNT 25 power source, the recommended argon shielding gas flow rate range is 10–15 liters per minute (L/min). If you are doing simple welding in a basic setup, remember that plasma cutting itself does not require this type of protective shield gas. The need for specialized shielding gases only arises when protecting an active weld pool from atmospheric contamination during the arc process.
Aluminum and Non-Ferrous Metals Demand Specialized Plasma Cutter Considerations
When customers ask, "Can you cut aluminum with a plasma cutter?", they are usually looking for consistency, which is where material knowledge becomes paramount. While most plasma cutters can cut aluminum, cutting non-ferrous metals presents unique value considerations related to heat expansion and arc stability that differ significantly from steel.
Aluminum requires careful setup because of its high thermal conductivity; it heats up and expands rapidly, which can cause distortion if the cooling rate is uneven. Plasma cutters handle this by generating intense energy to melt and expel the material quickly. The key difference you must account for when purchasing or renting a machine is that aluminum often necessitates maintaining optimal arc characteristics, sometimes favoring specific mixtures of shielding gases (like argon-helium mixtures) during an associated TIG process. Furthermore, if your cutting environment involves significant amounts of non-ferrous metal, be aware that the plasma cutter itself can generate splatter and residues that are difficult to clean compared to steel.
It is important to distinguish between materials that require only the primary high-heat arc (like aluminum) and those which benefit from additional gas stabilization. When doing TIG work on these metals, using a pure argon shielding gas ensures stable arc characteristics necessary for achieving structural integrity in the weld bead itself. If you are buying a machine primarily for cutting thin sheets of aluminum, ensure its power source can maintain a consistent flow that handles minor variations in material thickness without losing the critical 200–400 volts DC needed to start and sustain the arc.
The Total Cost of Ownership Is Determined by Consumables and Maintenance Schedules
A value consideration is rarely just about the upfront purchase price; it’s heavily tied to the total cost of ownership (TCO). This TCO includes not only consumables but also the necessary infrastructure upgrades, such as compressor maintenance or specialized gas regulator setup. You must factor in the ongoing costs associated with compressed air—the initial setup and required PSI range of 80–120 pounds per square inch (PSI)—and the actual volume consumption.
If you operate an older, less efficient machine, its poor duty cycle will force you to purchase a replacement or upgrade far sooner than necessary. Conversely, purchasing a system with reliable components that allow for easy replacement of consumable parts—like electrode tips and nozzles—will keep your operating costs low. When considering gas supply, the cost difference between utilizing pure argon versus an argon-helium mixture can be substantial over time, so understanding which shielding gas mix is required for your specific application (e.g., certain high-end TIG welds) is a core part of budget planning.
Furthermore, if you plan to integrate plasma cutting with other processes, like lift TIG welding, the machine's versatility becomes its value. Lift TIG uses a process where the tungsten briefly touches the workpiece and is then lifted to initiate the arc at low open‑circuit voltage; this sophisticated starting method reduces the risk of high-frequency electromagnetic interference with nearby electronics—a safety and operational benefit that adds significant long-term value by keeping your workspace functional.
Ultimately, when you are deciding on a plasma cutter, remember that the right choice is not the most powerful one available. It is the machine whose operating parameters—the required 80–120 pounds per square inch (PSI) air supply, the correct shielding gas flow rate for your TIG tasks (perhaps 10–35 cubic feet per hour for general TIG use), and a sufficient duty cycle for your typical material thickness—are perfectly balanced with the materials you cut most often. Never buy based on peak performance; always buy based on sustained, reliable output.
Your Compressor Is Part of the Purchase Price
Budget for the air supply before you budget for the cutter, because a 40 A air plasma machine that needs 80–120 PSI at roughly 5.3 cfm will expose a weak compressor faster than any spec sheet suggests. The failure mode is easy to recognize: the arc starts, cuts for a second or two, sputters, and dies mid-kerf, or the machine faults out on low-pressure. That is not a cutter defect. It is a compressor that can't hold pressure while the torch is flowing air continuously, and no amount of fiddling with the amperage dial fixes it.
Check your compressor's rated flow at pressure, not its tank size. A large tank buys you a few seconds of buffer and nothing else once the cut runs longer than the tank. Look at the pressure gauge while someone else pulls the trigger: if it sags below the machine's minimum while cutting, you need more compressor, a shorter hose run, or both. Small-diameter or coiled hose and undersized quick-connects rob pressure, and so does a clogged filter-regulator that hasn't been drained in months. Water in the air line is the other quiet killer — it reaches the torch, disrupts the arc, and eats electrodes early. A coalescing filter and a daily drain on the tank are cheap insurance compared with a consumable habit.
This is where the "cheap cutter" math collapses. A machine at the low end of the market paired with a compressor that can't sustain the required pressure is worse than a mid-range machine on a compressor that can. If your shop air is marginal, price a dedicated compressor into the decision before you compare cutter prices at all. If you can't justify the compressor, you can't justify the cutter.
Consumables and Duty Cycle Decide What the Machine Really Costs Per Cut
Price consumables by the set and by the cut, not by the piece. Electrodes and nozzles wear as a function of arc starts, pierce time, and how much you abuse the torch — dragging the tip on the plate, piercing thick stock at full amperage, or cutting with the wrong standoff all shorten life. A machine with hard-to-find or brand-locked consumables can cost more over a year of steady work than a machine with a higher sticker price and common parts. Before buying, find out what a full set of consumables costs and how many your local supplier stocks. If the answer is "we'd have to order them," that's a real operating cost in downtime.
Duty cycle deserves the same scrutiny. A machine rated at high amps with a short duty cycle will thermal-trip on a long cut or a run of repetitive cuts, and the clock doesn't stop for the operator standing there waiting for it to cool. That lost time is the hidden line item. If your work is mostly short cuts with breaks between them, a modest duty cycle is fine and the money is better spent elsewhere. If you're cutting nested parts for hours, buy duty cycle first and amperage second.
Match the machine to the thickness you cut every day, not the thickness you cut once. Cutting near a machine's maximum capacity is where consumable life falls off, cut quality drops, and the arc gets fussy — the machine is working at its limit and so are the parts. Running comfortably inside the rating is what keeps the consumable cost per cut predictable. That predictability, more than any single spec, is the value you're actually buying.
Consumable Interchangeability Is a Spec Sheet Line Nobody Reads
Ask the seller for the part numbers of the electrode, nozzle, and shield cup before you pay, then search those numbers. If they only resolve to the manufacturer's own store, you have bought into a consumable subscription, not a tool. The common torches take parts you can buy from more than one supplier, and that competition is what keeps your per-cut cost from drifting upward every year. A machine that saves a little on the sticker and then charges premium prices for brand-locked parts is the more expensive machine over a season of steady work.
Look at how the torch is built, too. A shielded torch with a drag-capable tip lets you rest the cup on the plate and cut without a standoff gauge — faster for thin sheet, less consistent on thick stock where you want a fixed standoff. Fine-cut consumables trade cut quality on thin material for a narrower kerf and less heat input, but they wear faster and don't like piercing. If most of your work is gauge material and light plate, fine-cut parts are worth stocking; if you cut structural stock all day, standard consumables last longer and you'll notice the difference in how often you're changing them.
The tell that you bought the wrong torch, not the wrong machine, is consumable life that drops off a cliff when you move up in thickness. Electrodes eroding early on thick cuts usually means you're piercing at full amperage, holding too long a pierce, or dragging the tip. Change the technique before you change the machine.
Don't Buy a Cutter to Do a Saw's Job
Plasma is the wrong tool for straight cuts in thick plate and for anything where the cut edge has to be a finished surface. The kerf is wider than a saw's, the edge carries a slight bevel and a heat-affected zone, and the dross on the bottom has to be knocked off or ground. If your work is mostly cutting bar stock, plate to length, or clean square edges, a cold saw or a bandsaw will give you a better edge, no air supply, and no consumables — for less money up front. The plasma earns its place when you need curves, pierced holes, or cuts in material a saw can't easily clamp.
The heat is the other cost. Cutting aluminum and thin steel with plasma puts a heat-affected zone along the kerf, and on thin material that means warp if you cut fast and let the part cool unevenly. Sequence your cuts so the heat stays balanced — cut opposing sides in rotation rather than running one long cut down the middle of a sheet — and let the part cool before you clamp and weld it. On aluminum, the cut edge also needs a clean-up before welding; the oxide layer and any residue from the cut have to come off or you'll chase porosity in the weld.
Where the cutter earns its keep is in the shop that already has the air, cuts a mix of shapes, and needs a fast, clean-enough edge that gets finished later. Buy it for that job. Don't buy it to replace a saw you should have kept.