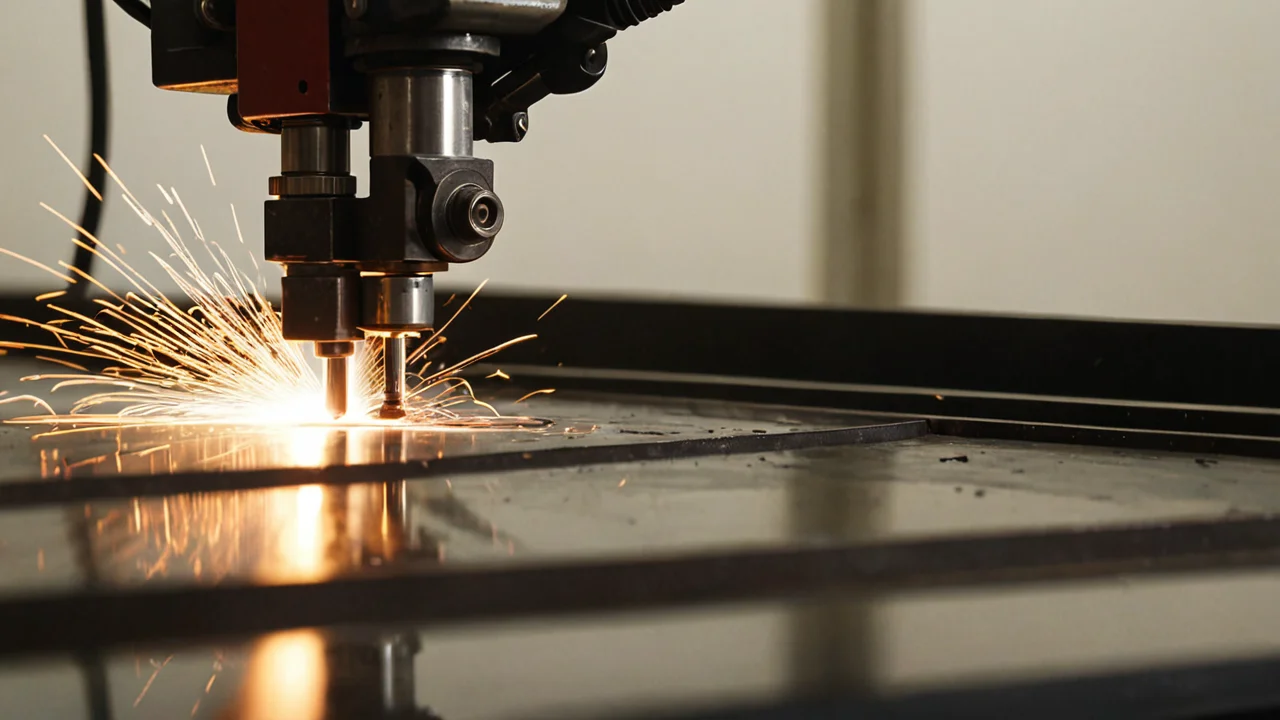
For general structural fabrication or rapid removal of thick material, I would pick plasma cutting; for anything requiring fine detail, complex joints on stainless steel, or repeatable high-integrity welds where appearance matters more than speed, nothing touches TIG welding. The fundamental difference boils down to energy source: plasma uses a superheated gas stream driven by compressed air and electricity, acting like an abrasive jet torch, while TIG is a highly controlled arc process that uses inert shielding gases (like pure argon) to keep the weld pool pristine.
Plasma Mechanics
A plasma cutter works on incredibly simple yet brutal physics: it takes electricity, compresses ambient air, and forces that stream through a constricted orifice to create an extremely hot, ionized gas—the plasma. At its core, a plasma cutter is essentially a controlled jet of superheated air capable of reaching temperatures high enough to melt most metals. It doesn't rely on filler rod addition like some other welding processes; instead, it uses the directed energy and the physical force of the stream itself to cut through material.
When you first start operating one—if you are wondering how to operate a plasma cutter—you need to understand that the process requires specific inputs. You must maintain a compressed air supply pressure range between 80–120 pounds per square inch (PSI) for something like a 40 A unit, which generates an approximate airflow rate of 5.3 cubic feet per minute (cfm). This gas flow isn't just for the cut; it is the medium that carries the heat and provides the physical momentum to separate the molten metal from the parent material.
The actual cutting action relies on electrical principles, requiring a common DC voltage range between 200–400 volts DC to initiate and maintain the arc. This electric current excites the gas stream (usually compressed air), causing it to ionize—that is, stripping electrons from the atoms of the gas molecules. Once ionized, the gas becomes plasma: an electrically conductive state that transmits intense thermal energy in a highly focused jet. The combination of extreme heat and directed kinetic force allows it to cut aluminum as well as steel or mild steel.
However, when people ask does a plasma cutter need gas, the answer is yes—it needs two types: the primary propellant (the compressed air that creates the stream) and often, if cutting specialty materials, an auxiliary shielding gas. The process inherently uses the ambient air as its fuel source to create the superheated jet. Because the energy delivered by this controlled plasma arc is so intense, it vaporizes metal through a combination of thermal transfer and mechanical pressure.
TIG Welding Fundamentals
In stark contrast to the brute force of plasma cutting, TIG welding (Gas Tungsten Arc Welding, GTAW) is an art of precision. This process involves using a nonconsumable tungsten electrode to create an electric arc while simultaneously surrounding the molten weld pool with a protective sheath of inert gas. The primary goal of this method is not just to join two pieces of metal, but specifically to prevent atmospheric contamination—from oxygen, nitrogen, or water vapor—which would otherwise cause porosity and significant structural defects.
The shielding gas used in TIG welding is critically important. Pure argon is the noble gas most commonly supplied because it offers excellent arc stability and minimal reactivity with common metals. While 100% argon is preferred for its purity (usually provided at around 99.99% or higher), sometimes argon-helium mixtures are utilized depending on the thickness and material being joined. The system requires a precise flow rate; for example, recommended argon shielding gas flow rates for TIG welding on an LNT 25 power source fall within the range of 10–15 liters per minute (L/min).
Unlike plasma cutting, which uses compressed air as its propellant, TIG relies solely on controlled electric energy and inert gases. When you use shielding gas in TIG, it does not participate in the cutting; rather, it acts as a sterile bubble around the joint, keeping everything molten and perfect until solidification.
Process Comparison
The mechanical difference between these two processes can be summarized by their energy delivery. Plasma is an energetic jet that ablates material rapidly. TIG, conversely, is a highly controlled thermal deposition process where the arc provides heat, and the shielding gas ensures quality.
When comparing them head-to-head, keep these operational details in mind: A plasma cutter requires high PSI of compressed air (80–120 pounds per square inch for a 40 A unit), generates extreme cutting force, and is excellent for quick, rough passes through thick materials. TIG welding, conversely, manages precise heat input across the entire weld bead; it's designed for structural integrity where minimizing distortion and achieving aesthetic quality are paramount.
I often find that if a job requires you to join two components—even if one of them is very dirty or oxidized—TIG provides a far cleaner, more dependable joint because its reliance on the inert gas shield makes it less susceptible to environmental contamination than open-air cutting techniques. While both methods can certainly cut aluminum (with plasma using high voltages and TIG being excellent for precise aluminum welding), the final mechanical output is fundamentally different: raw separation versus controlled fusion.
Operational Trade-offs
Understanding how to use a plasma cutter effectively means acknowledging its limitations. While it’s incredibly versatile for rapid material removal, the extreme heat and pressure involved mean that residual stress can be significant on thinner or complex geometries. The intense thermal cycling of plasma cutting makes it inherently more difficult to control precisely compared to TIG.
Conversely, while TIG offers unparalleled quality—it is frequently used when a high-quality weld is required on metals such as steel, stainless steel, and aluminum—the process demands significant setup time and expertise. It is slower than plasma cutting for sheer material removal volume. Furthermore, the equipment required to maintain proper shielding gas flow rates (like 10–35 cubic feet per hour for TIG with argon) adds cost and complexity compared to simply running a compressed air line.
The choice ultimately hinges on your priority: Do you need speed and material removal power that can handle dirty, complex edges? Use plasma. Or do you need the highest possible weld integrity, minimal heat distortion, and a finish that looks like it came from a specialist shop? Then TIG is the way to go.
Why Your Air Supply Is the First Thing to Fail
If a plasma torch cuts well for a few seconds and then sputters, loses the arc, or leaves a heavy dross bead on the bottom edge, the consumables are usually innocent. The air line is the suspect. A 40 A air plasma cutter wants a supply held between 80–120 pounds per square inch (PSI) and flowing at roughly 5.3 cubic feet per minute (cfm), and it wants that pressure held while the arc is running, not just at the regulator with the trigger off. Most small-shop failures are dynamic pressure drops: a compressor rated for the cutter's consumption, a long coil hose with a small inside diameter, and a quick-connect that has been beaten up for years. The gauge reads fine static, then sags the moment the solenoid opens.
Put a gauge at the machine's inlet, not at the compressor, and watch it during a cut. If it sags below the machine's required band, shorten the hose run, upsize the fittings, or add storage capacity at the cutter. Water is the second killer. Compressed air in a humid shop carries moisture into the torch, and you notice it as a rough, inconsistent cut, a greenish tint on the electrode, or pitting on the nozzle orifice. A coalescing filter and a drip leg at the lowest point of the run cost little and buy you a lot of consumable life. Drain the tank regularly — a compressor that sits with condensate in it pushes that water straight to the torch.
The honest trade-off: air plasma is cheap to run and needs no bottle rental, but it is a dirty process. The cut face oxidizes, and on stainless or aluminum the cut edge is not weld-ready without grinding back past the nitride layer. If you are cutting parts that will be welded, budget the cleanup time or move to a machine with a shielding gas option. Air is the right choice for structural steel, demolition, and rough fabrication where speed beats edge quality.
Matching the Consumable to the Cut, Not the Machine
Plasma consumables are a matched set — electrode, swirl ring, nozzle, and shield — and mixing a worn electrode with a fresh nozzle is a false economy that shows up as a ragged kerf and short nozzle life. The electrode's hafnium insert erodes with every arc start, so on thin material where you are piercing constantly, electrode life falls off a cliff compared to cutting plate. If you are doing a lot of short cuts on sheet, expect to change electrodes far more often than someone cutting thick plate with long, continuous travel.
Set the cut height with a drag shield or a standoff guide rather than by eye. Too high and the jet spreads, the kerf widens, and dross forms on the bottom; too low and you risk a collision that destroys the nozzle in one touch. Pierce height matters even more: start the arc above the plate, let it establish, then drop to cut height. Piercing at cut height on thick material blows molten metal back into the nozzle. On material thick enough that a straight pierce is risky, start at the edge instead.
Cut speed is the variable most people get wrong, and the symptoms are readable. Too slow and you get a heavy, bubbly dross that is hard to chip off, plus a widening kerf and heat discoloration spreading well past the cut line. Too fast and the arc lags behind the travel, leaving a beveled, incomplete cut with dross clinging at the bottom corners. The correct speed gives you a cut face with a slight drag angle and sparks exiting nearly straight down. Learn to read the sparks: they tell you more than the spec sheet.
- Ragged top edge with a rounded kerf: consumables worn or cut height too high.
- Dross that welds itself to the bottom: travel too slow, or amperage too high for the thickness.
- Arc dies mid-cut: check inlet pressure during the cut before replacing anything.
- Hard, glassy dross on stainless or aluminum: normal for air plasma; grind back before welding.
Starting the Arc: Where TIG Setup Actually Bites
Arc starting is where TIG punishes sloppy setup, and it is the first place to look when a machine that welded fine yesterday refuses to strike cleanly. If your power source uses lift TIG starting, you touch the tungsten to the workpiece at low open-circuit voltage and lift to initiate the arc. It avoids the high-frequency interference that scrambles nearby electronics, but it means the tungsten contacts the metal on every start, and a dipped or contaminated tungsten produces a wandering, split arc. Keep a dedicated grinding wheel for tungsten, grind lengthwise, and re-point whenever the arc starts hunting.
Gas flow is the other half of clean starts, and more is not better. Argon flow for TIG typically runs 10–35 cubic feet per hour depending on cup size and joint type, and on an LNT 25 power source the recommended range is 10–15 liters per minute. Too little flow and you get porosity and a sooty, grey bead; too much and the gas stream turns turbulent, aspirating room air into the shielding envelope and giving you the same porosity you were trying to avoid. Set flow with the gas flowing through the torch, not at a dead regulator, and add a few seconds of post-flow so the tungsten and pool cool under gas rather than air.
The cost side is real: pure argon at welding-grade purity — around 99.99% or higher — means a bottle, a regulator, and a rental or lease, whereas plasma cutting runs off the shop compressor you already own. That is the trade you are making. TIG buys you a controlled thermal process with a sterile gas envelope and a weld that needs no cleanup; plasma buys you speed on a gas line you probably already have. Neither is the wrong answer — but the failure modes are different, and knowing which one you are looking at saves more time than any spec sheet.