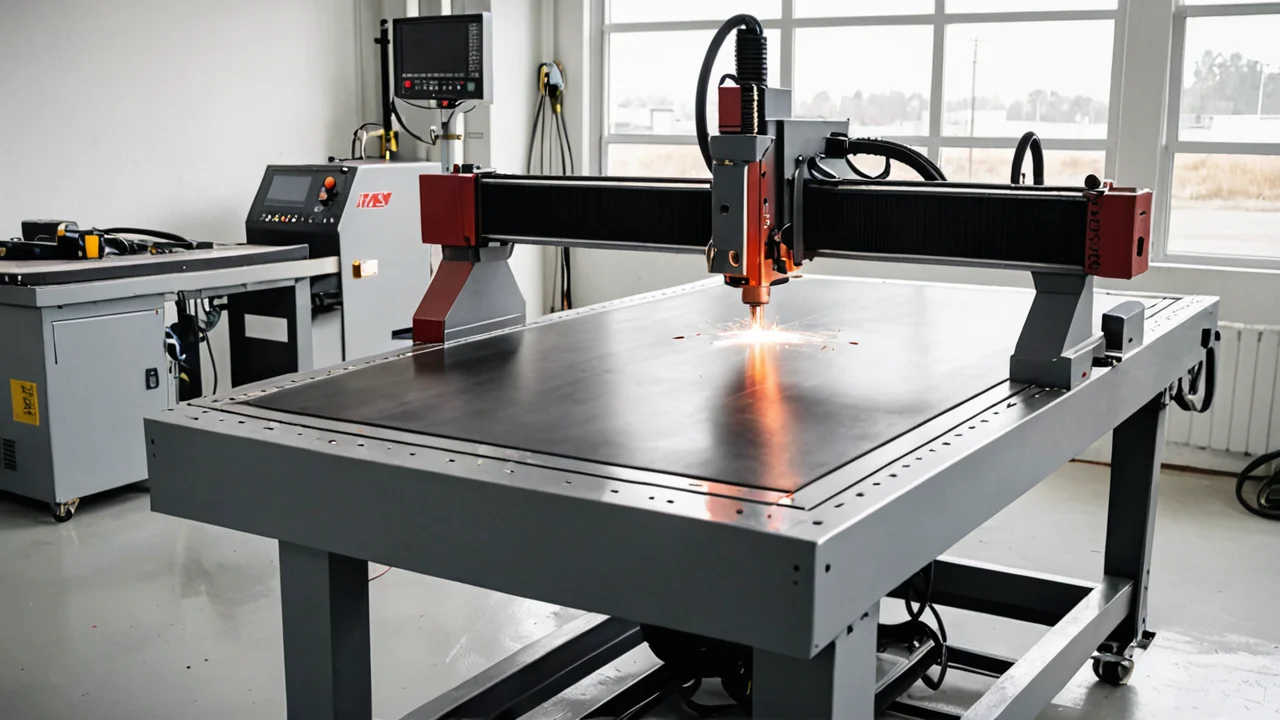
For achieving true precision with CNC plasma cutting, do not prioritize simple cost savings; instead, focus your selection entirely on a table that provides exceptional vertical rigidity and flatness across its working surface.
A high-quality CNC table for precision work must minimize deflection under the load of the gantry system, especially when processing reactive metals like aluminum. While plasma cutters require steady power—operating within a common DC voltage range of 200–400 volts DC—the primary structural concern is maintaining a perfectly level and stable plane to ensure that the cutting torch remains at consistent Z-axis height regardless of material thickness or run length.
Measure your workspace requirements first
The initial step in selecting plasma table infrastructure is determining not just the maximum footprint you need, but also the required working envelope relative to common operational setups. Since precision work often involves handling sheet metal that may require specific support structures—like jigging or clamping mechanisms for stainless steel or thicker aluminum sections—the available surface area must comfortably exceed your planned cuts by at least 20%.
Furthermore, remember that while the cutter itself has a specified operational air requirement—such as needing an air supply pressure range of 80–120 pounds per square inch (PSI) for a 40 A unit—the table's electrical infrastructure must account for auxiliary components like compressors, gas regulators, and vacuum systems. This means that the overall machine footprint calculation needs to encompass utility hookups as much as the actual cutting bed.
It is crucial to realize that while plasma cutters are versatile enough to handle aluminum, their performance relies heavily on a steady supply of compressed air; for example, running at 80–120 pounds per square inch (PSI) will generate an approximate air flow rate of 5.3 cubic feet per minute (cfm) from a 40 A cutter.
Match the table’s rigidity to your material load
When working with materials that demand high precision, such as thin gauge stainless steel or highly reflective aluminum, the choice of supporting structure is paramount. Plasma cutting works by generating a high-velocity arc plasma stream that superheats and blows away metal contaminants; this process generates significant localized thermal stress on the workpiece.
If you opt for a table made from cast iron or heavily laminated steel, investigate its torsional stiffness. For maximum precision, the table should be designed to dampen vibration rather than merely withstand load. While plasma cutting is inherently different from TIG welding—which uses an inert gas like pure argon (typically 99.99% or higher) and requires specific shielding practices—both processes demand absolute stability from the foundation up. A wobble in the table translates directly into a deviation on the cut part.
However, be aware of trade-offs: ultra-rigid tables often require more specialized installation, potentially complicating integration with existing utility lines. If your primary process is consistently plasma cutting thicker sections, a simple sheet metal fabrication shop floor may suffice; but if you are working on intricate, thin profiles requiring high dimensional accuracy, the rigidity becomes non-negotiable.
Integrate power requirements accurately
The electrical demands of a CNC plasma cutter table setup go far beyond just powering the cutting head. You must account for the primary power source required to maintain the arc (operating within a common DC voltage range of 200–400 volts DC), alongside auxiliary equipment.
A major oversight is undervaluing the gas supply system. While TIG welding, which uses inert shielding gases like argon, might require flow rates between 10–35 cubic feet per hour (cfh) for general use or 10–15 liters per minute (L/min) on a specific power source, plasma cutting requires high-volume compressed air. Ensure your table setup can accommodate multiple regulators and lines necessary to feed the primary plasma cutter system.
When sourcing quotes, insist that electrical capacity assessments include not just the machine motor loads but also the peak draw of the gas and compressor units. A common mistake is selecting a table with excellent structural integrity but insufficient integrated power distribution for all supporting peripherals.
Evaluate alternative support surfaces
Depending on whether you are plasma cutting flat sheet stock or performing intricate, three-dimensional work, the "table" itself might not be the final component. For optimal precision, consider adding specialized material supports that complement the primary working surface.
If your work involves complex geometries where a simple bed cannot provide sufficient support—for instance, mounting pieces that require precise fit-up before cutting—you may need to integrate an articulating fixture system directly into the table’s frame. These fixtures must be designed with materials and load capacities appropriate for the highest pressures generated by the plasma torch during operation.
When comparing options, remember that while some basic workbenches might offer a cheaper initial outlay, their lack of standardized flatness tolerance can lead to unacceptable dimensional errors. For precision, investing in a table built specifically around gantry movement and proven flat surfaces is always worth the cost differential.
Optimize for minimal thermal distortion
Plasma cutting generates intense heat that, if not managed, will warp the workpiece or surrounding fixture materials, ruining any precision effort. The primary goal of a high-precision table design must therefore be to provide rapid and uniform cooling pathways or to support materials that are inherently stable.
When plasma cutting aluminum—a material known for its thermal conductivity—the speed at which heat dissipates is critical. If the table surface itself acts as a heat sink but does not allow sufficient airflow around the cut area, localized warping can occur. Therefore, ensure the chosen setup allows for necessary clearance between the workpiece and the table’s supporting frame.
Keep in mind that while other processes like TIG welding require meticulous gas management—using 100% argon or argon-helium mixtures to protect the weld pool from atmospheric contamination—plasma cutting's challenge is managing the heat transfer after the cut. The structure must be robust enough to absorb vibration without transmitting excessive thermal movement back into the material.
Slat bed design decides your cut quality more than the gantry does
Specify a slat pitch and slat thickness that match the thinnest material you actually cut, not the thickest. A bed spaced for heavy plate leaves thin sheet unsupported between slats, and the moment the arc pierces, the sheet sags into the gap and the kerf goes out of square. For precision work on thin gauge, tighter slat spacing with thinner, easily replaced slats beats a heavy-duty bed built for thick plate — and the consumable slats are cheap to swap when they erode.
Ask the builder how slats are retained. Drop-in slats in notched rails let you replace a worn section in minutes without pulling the whole bed; bolted or welded slats turn a routine maintenance job into a half-day. Slats erode fastest directly under the pierce points, so plan to rotate and flip them on a schedule rather than waiting for a cut to fail. If you notice dross concentrating on one side of the kerf and the torch height looks correct, look down: a slumped slat section is tilting the work.
The trade-off is real. Tight slat spacing costs you airflow and makes dross cling to the slats, and it limits how much of the bed you can use for heavy plate before the slats themselves become the wear item. If your work is split between precision thin sheet and occasional thick stock, a bed with removable slat cassettes — one fine-pitch set, one coarse — is worth the extra cost over a single compromise bed.
Torch height control and the Z axis are where precision is won or lost
Insist on a torch height control that senses the workpiece before every pierce, not a fixed-height setup. A THC that probes the plate, retracts to a pierce height, then drops to cut height compensates for slat wear, warped sheet, and the slight bow a thin sheet takes as it heats. Without it, the arc voltage you tuned on the first part drifts by the end of the nest and the kerf widens. Verify the Z axis has enough travel to clear the tallest fixture you plan to use plus the retract distance — a short Z column is the most common reason a table that cuts flat sheet well cannot handle a raised fixture.
Watch the drive on the Z axis specifically. A fast, rigid Z with a floating head and a breakaway mount protects the torch when a tip-up catches the shield; a rigidly mounted torch with no breakaway will snap or bend on the first tip-up, and you will not notice until the next cut runs crooked. Ask whether the breakaway is mechanical or magnetic and how it re-homes after a trip.
Because the arc runs at a common DC voltage range of 200–400 volts DC, keep the torch lead routing and the height-sensing wiring separated. Sensing leads run alongside a high-voltage arc lead is a classic source of erratic height readings that mimic a bad THC. If the torch bobs or dives only on certain parts of the bed, suspect cable routing before you replace the controller.
The honest cost here: a probing THC and a rigid, breakaway-equipped Z add to the price and add setup steps to every job. On a table dedicated to one thickness and one nest, a fixed height can hold tolerance. It falls apart the moment material thickness or flatness varies, which in a job shop is most days.
Air supply and dry gas are part of the table, not an afterthought
Size the compressed air system to the cutter's demand at pressure, and then dry it. A 40 A air plasma cutter wants an air supply pressure range of 80–120 PSI and pulls roughly 5.3 cfm at that pressure, so a small shop compressor that also feeds other tools will starve the cut mid-kerf and leave a ragged edge. Budget for a refrigerated dryer and a coalescing filter at the machine; moisture in the air shows up as porosity-like pitting on the cut face and shortens electrode life, and it is far cheaper to fix at the filter than to chase as a cut-quality problem.
Route the air line to the table with its own regulator and gauge at the inlet, so you can read the pressure the torch actually sees rather than the pressure at the tank. Pressure drop across a long, undersized hose is the usual reason a cutter set to a healthy line pressure still cuts poorly. Keep a spare filter element on the shelf and change it on a schedule — a saturated element passes water and you will not see it until the electrodes start dying early.
For comparison, TIG welding on the same shop floor runs shielding gas at 10–35 cubic feet per hour with argon, or 10–15 liters per minute on a specified power source. Those are small, steady flows from a regulated cylinder. Plasma air is a high-volume, continuous demand from a compressor, and the table's utility planning has to treat them as different animals — one cylinder regulator will not feed a plasma torch, and one undersized compressor branch will not keep a precision cut clean. If your shop runs both processes, give the plasma cutter a dedicated drop and let the TIG station keep its own regulated argon supply.
Grounding and work-lead practice on a precision table
Run the work lead to the workpiece itself, not to the table frame, and clamp it as close to the cut as the gantry allows. The slats are a poor conductor path — they are consumables, they erode, and a slat-to-frame joint that looks tight will develop resistance as oxide builds up. When the return path is long or intermittent, the arc hunts for ground, cut edges go ragged on one side, and the THC reads voltage it cannot trust. You will notice it as a kerf that is clean at the start of a nest and rough by the end, on the same material and the same settings.
Bond the table frame to the shop ground independently of the work lead. CNC electronics, the height-sensing circuit, and the drive motors all share that frame, and a floating frame turns the whole bed into an antenna. The symptom is a machine that cuts fine and then throws an unexplained fault mid-nest. Keep the work clamp and its cable in good condition — a frayed clamp cable is cheap to replace and expensive to diagnose around.
This costs you a few minutes of clamp placement on every job and some cable management. On a table running one nest of one material all day, clamping to a slat and leaving it is tempting. It works until it doesn't, and the failure mode is a scrapped part rather than a stopped machine.
Nesting and lead-in strategy for the tolerance you actually need
Set lead-ins off the finished edge and into the scrap side of the kerf, and give the pierce its own dwell before the cut profile starts. A pierce is the dirtiest moment in the cut — the arc blows molten metal back up and the kerf at the pierce point is always wider than the steady-state kerf. If your lead-in runs straight into the finished contour, that widened zone lands on the part and shows up as a divot at the start of every profile. The fix is free: move the lead-in, lengthen it, and add an arc-on delay so the pierce completes before motion begins.
On thin sheet, sequence nested parts so the torch is not cutting a profile next to a section that has already lost its support. Cut the parts that share a slat gap in an order that leaves material under the torch, and keep the outermost profiles last. You can see the result of getting this wrong as a bow or a scrapped part near the end of a nest, with no change in settings to explain it.
None of this is a table specification, which is the point. Two shops with identical tables will get different tolerance off the same nest based on clamp placement, lead-in geometry, and cut order. Buy the rigidity, the probing THC, and the fine-pitch slats — then spend the setup time on the software side, because that is where the last of the precision comes from.