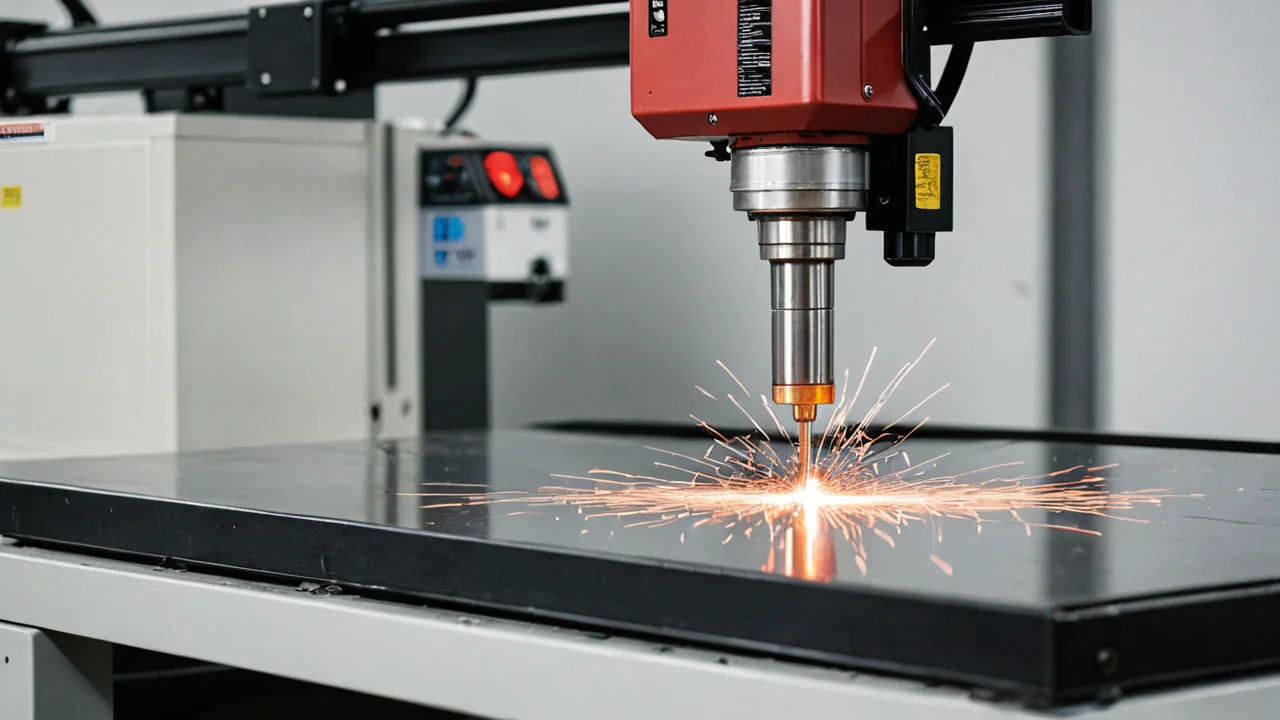
If you are consistently fabricating structural steel parts up to 1/2 inch thick at a job site, do not select a model rated only for light duty; you must opt for a machine with robust power output and enough operational range to handle the required pressures, which typically fall between 80–120 pounds per square inch (PSI) for even a 40 A air plasma cutter.
The Right Cutter Is Determined by Material Thickness and Required Precision
Choosing the right commercial plasma cutter is fundamentally about matching the machine's rated capacity—in terms of amperage, duty cycle, and operational voltage range—to the thickest material you intend to cut and the required edge finish. While many entry-level units are marketed as universal solutions, they often compromise significantly on one end or the other; for instance, a unit optimized purely for thin sheet metal might struggle with deep penetrations in thicker plate, leading to excessive kerf widening or machine stalling. You need to look past the advertised maximum amperage and instead evaluate the specific duty cycle rating at that current, ensuring it matches your anticipated cutting time relative to material thickness.
The trade-off here is clear: power equals capability, but also cost and complexity. A smaller, more portable unit will be cheaper than a large industrial benchtop setup, but that portability often means sacrificing the ability to maintain stable arc performance when encountering varied materials or geometry changes across the job site. When you are dealing with structural work in steel or stainless steel—the primary domain of plasma cutting—you must prioritize machines designed for continuous operation and deep penetration, even if they add weight and cost.
However, it is crucial to remember that plasma cutting is a destructive process; unlike processes such as TIG welding (Gas Tungsten Arc Welding, GTAW), which produce precise, high-quality welds on metals such as steel, stainless steel, and aluminum by using an inert shielding gas like pure argon around the weld pool, plasma cutting leaves a cut path. This means that if your final product requires structural integrity or aesthetic perfection at the cut line—for example, for components that will be re-welded later—plasma is not the endpoint process; it is merely a preparation step. If precision welding quality is paramount, you must consider adding TIG capabilities to your overall shop setup.
Plasma Cutting Works By Creating a Highly Concentrated Arc Jet
In simple terms, a plasma cutter operates by generating an extremely hot, constricted gas stream—the "plasma"—which acts as an intensely energetic cutting torch. The machine's core function is to convert electricity into this highly concentrated energy jet capable of rapidly melting and blowing through conductive materials. This process requires the initial establishment of an electric arc; specifically, a common DC voltage range required to start and maintain this arc falls between 200–400 volts DC.
The mechanism relies on forcing an inert gas—usually compressed air or nitrogen—through a constricted orifice within the torch head. When sufficient voltage is applied across this gap, the gas rapidly heats up, ionizing into plasma (a superheated ionized gas). This resulting jet of energy has enough thermal intensity to melt the base metal and provide enough kinetic force to blow through it using an accompanying auxiliary gas stream. The overall operation involves maintaining a stable arc while simultaneously delivering high-pressure air to achieve the cut.
Understanding how this works helps clarify that plasma cutting is fundamentally a process of material removal, not material joining. When you are trying to understand 'how does plasma cutter work,' think less about heat transfer for welding and more about controlled excavation using immense thermal energy coupled with pneumatic force. The machine’s ability to regulate voltage and maintain a stable gas flow rate at high pressures is what dictates the quality of the cut and the ease of operation.
You Must Maintain Specific Pressures and Flow Rates for Stable Operation
Operational stability in plasma cutting is entirely dependent on maintaining precise pneumatic parameters, which directly influence the quality of the cut. The single most critical metric to monitor is system pressure; for example, a 40 A air plasma cutter requires a compressed air supply pressure range between 80–120 pounds per square inch (PSI). Dropping below this required range will cause unstable arc performance and irregular kerf width.
Once the optimal PSI is achieved, the system must maintain an appropriate flow rate. For the aforementioned 40 A cutter operating within the specified pressure range, the approximate air flow rate needed is 5.3 cubic feet per minute (cfm). These specific figures are non-negotiable; using a regulator or compressor that cannot reliably deliver this precise flow and pressure will result in poor cuts, arcing instability, and premature wear on the torch consumables.
It is also helpful to compare these requirements to related processes. While TIG welding uses different gases—such as pure argon (typically supplied around 99.99% or higher) for stable arc characteristics—its gas flow rates are measured differently, ranging from a recommended 10–15 liters per minute (L/min) when using an LNT 25 power source. Plasma, however, is overwhelmingly pneumatically driven. Therefore, while both processes require controlled gas delivery, the plasma cutter’s dependence on high-PSI compressed air makes compressor quality and maintenance arguably more critical than for a standard TIG setup.
Plasma Cutting Is Suitable for Aluminum But Requires Careful Parameter Adjustment
Yes, plasma cutters can cut aluminum; however, it is vital to understand that the process is highly material-specific and requires careful selection of operating parameters. When cutting aluminum, you are dealing with a metal that has significantly higher thermal conductivity than steel, meaning heat dissipates rapidly. This demands that the machine maintain optimal voltage settings and potentially adjust gas mixtures or flow rates compared to when it cuts mild steel.
The general question regarding 'can you cut aluminum with a plasma cutter' requires a nuanced answer: yes, provided your machine is rated for the specific application and has the necessary control capabilities. Failure to adjust parameters will result in excessive heat build-up at the cutting edge or an unstable arc that struggles to penetrate the material consistently. For optimal results on conductive materials like aluminum, ensuring that the entire system—from the compressor tank down to the torch head—is clean and free of residues is paramount.
It must be noted that plasma cutters are not limited to certain metals; they can cut a wide range of conductive materials. The only material limitation often encountered is related to non-conductive items or extremely complex geometries where excessive heat build-up might warp the workpiece before the plasma jet can achieve clean penetration. For instance, if your task requires achieving an aesthetically perfect finish on aluminum that needs to survive subsequent welding processes, a skilled welder will invariably recommend TIG welding as the superior method of execution rather than relying solely on the cut itself.
Choosing a Commercial Unit Means Balancing Power Density Against Portability
Ultimately, selecting a plasma cutter involves balancing raw cutting power (amperage and PSI) against the logistical constraints of your job site—specifically, how often you need to move the unit. If your work is confined to one large workshop area where material sizes are consistent, prioritizing maximum continuous duty cycle and high voltage capability makes sense, allowing for the use of heavier, more robust industrial units. Conversely, if your needs involve moving between multiple outdoor or temporary sites daily, a lighter, lower-amperage unit that still meets the minimum requirements (like maintaining 80–120 PSI) is the superior choice, even though it means slower cutting speeds and reduced thickness capacity.
A key aspect of this selection process is considering the overall system components. Do you need just the cutter torch head attached to a power source, or do you also require an integrated air compressor? If portability is key, ensuring that the power unit can operate efficiently from either grid electricity or gas/air sources—and critically, confirming the appropriate PSI delivery mechanism—is more important than the peak amperage rating alone. Remember that the arc voltage required (200–400 volts DC) must be achievable and stable regardless of how many feet away your cutting point is.
When you evaluate different brands or models, do not only look at the maximum advertised power; instead, seek documentation detailing the actual operational performance curve across various thicknesses. This will reveal where the machine begins to degrade in efficiency, which is precisely when a job site application might fail unexpectedly. A professional approach requires viewing the plasma cutter as part of an integrated system—the source, the regulator, and the torch—and ensuring that all three components are rated for your most demanding cutting scenario.
Consumables and Air Quality Are Where Cheap Machines Fail First
Before you compare amperage ratings, look at the torch consumable stack and the air you plan to feed it. The electrode, nozzle, swirl ring, and shield are a wear item, and on a machine with a proprietary torch you are locked into that brand's parts pricing for the life of the unit. A cutter that shares a common, widely stocked torch style is worth more in practice than one with a slightly higher amp rating and a captive consumable supply.
Water and oil are the quiet killers. An air plasma cutter running on a compressor with a wet tank will pit the electrode, widen the nozzle orifice, and give you a cut that starts clean at the beginning of the plate and raggedly bevels by the end. You notice it as an arc that wanders, a kerf that widens across a single cut, or a torch that needs increasing standoff to keep going. A coalescing filter and a refrigerated or desiccant dryer ahead of the machine cost real money, but they extend consumable life and hold cut quality far better than upgrading to the next size power source.
Duty cycle is the other spec that bites. A machine rated for continuous work at one amperage will be rated for a lower percentage at its peak. If your jobs are long straight cuts on thick plate rather than short bracket work, buy the duty cycle you need at the thickness you actually cut, not the headline maximum. Thermal shutdown mid-cut on a structural part is not a minor annoyance; it is a scrapped workpiece.
The Air Supply Is a System Decision, Not an Accessory
Size the compressor to the cutter's demand at pressure, not to the cutter's nameplate. A 40 A air plasma cutter needs a supply held between 80–120 pounds per square inch (PSI) and roughly 5.3 cubic feet per minute (cfm) at that pressure. That cfm figure is the one people ignore: a compressor with a large tank but a small pump will hold pressure at rest and then sag the moment the arc starts, and the sag is what destabilizes the cut.
Work through it in order. Decide the thickest material and the amperage that requires. Read the required PSI and cfm from the manual. Then check your compressor's rated cfm at that pressure, not its tank size and not its peak cfm at zero pressure. Add filtration and drying between the compressor and the machine. Only then choose the cutter. Doing it in the other order is how shops end up with a capable machine fed by an undersized compressor and blaming the torch.
Portability cuts against this. A machine that runs from a jobsite compressor is only as portable as that compressor, and a small gas-driven unit may not sustain the flow a larger cutter wants at pressure. If you move between sites daily, accept a lower-amperage machine that your air supply can actually feed, or budget for a compressor sized to the cutter. The power side matters too: the arc needs a common DC voltage range of 200–400 volts DC to start and hold, and long runs or marginal supply will show up as hard starting and a weak jet.
The honest trade-off is that a well-fed mid-size cutter with clean, dry air and a common torch will outcut a bigger machine on a wet, starved supply every time. Spend the money on air treatment and consumable availability before you spend it on amps.