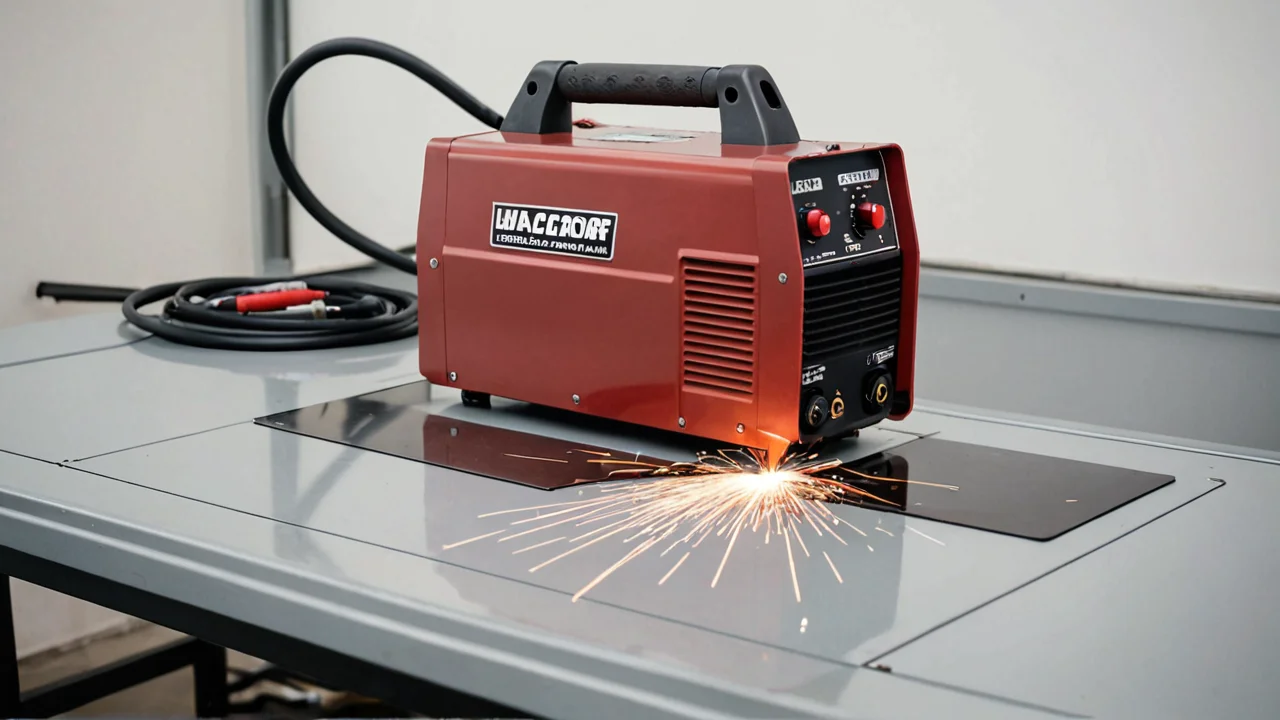
A portable plasma cutter uses electricity to generate a superheated, high-velocity gas stream—the plasma—that acts as a highly directional thermal beam capable of cutting through various metals with relative ease.
Plasma Cutting Basics
At its core, a plasma cutter is essentially an advanced torch that converts electrical energy into extreme heat and pressure. It does not use oxy-fuel gases like traditional gas cutting torches; instead, it uses electricity to ionize a primary shielding gas (such as air or nitrogen) through an electric arc. This process creates the plasma—a superheated gas composed of free electrons and ions—which can reach temperatures far exceeding those required for clean material severance. The equipment itself includes a power source, a torch assembly with electrodes, and often requires an external compressed air supply.
The fundamental action involves creating an electric arc between the electrode and the workpiece. To successfully initiate and maintain this process, the system must operate within a common DC voltage range required to start and maintain a plasma cutting arc of 200–400 volts DC. The torch design and power unit are calibrated to deliver sufficient amperage while managing this volatile electrical discharge.
The entire operation requires more than just electricity; the process uses a gas—typically air or nitrogen, depending on the required cleanliness and material—to serve as the working fluid that forms the plasma stream. This is what allows it to cut materials quickly and effectively, making it highly versatile for field use.
Operational Requirements
Operating a portable unit involves setting up both the electrical power source and the pneumatic supply. The machine must be fed compressed air at sufficient pressure. For instance, running a 40 A air plasma cutter requires a steady input of compressed air within the range of 80–120 pounds per square inch (PSI). This minimum pressure is crucial because it dictates both the force behind the cutting arc and the consistency of the material removal.
Once these inputs are stable, the operator positions the torch to create a gap between the electrode and the metal. The electrical circuit then closes, establishing the continuous plasma stream. The actual technique involves maintaining a consistent travel speed while guiding the torch through the cut path, managing the angle of attack to ensure that the high-velocity gas stream cuts cleanly through the material cross-section.
It is vital to remember that while plasma cutting is generally fast and effective, it is not without its physical limitations. The required pressure and electrical input mean that portable units must be robustly maintained; fluctuations in either supply can cause unstable arcs or premature electrode wear, resulting in poor cut quality characterized by excessive splatter or incomplete cuts.
Material Compatibility
While plasma cutters are marketed as highly versatile tools capable of cutting many materials, their performance is not uniform across all metals. They perform exceptionally well on common structural steels and mild steel sections due to the heat intensity delivered by the plasma arc. However, when dealing with specific alloys like aluminum, the process introduces unique challenges that require careful setup.
The question of whether a plasma cutter can cut aluminum is answered affirmatively; in fact, it does cut aluminum. But achieving a clean, predictable cut requires acknowledging the material's thermal properties. Aluminum has different melting and vaporization characteristics compared to carbon steel, meaning the optimal cutting speed and gas type must be adjusted.
For materials like stainless steel or thicker structural alloys, the system must balance power output with heat dissipation. While plasma provides immense localized heat, excessive exposure can distort certain metals. Therefore, even when using a machine designed for field work, the trade-off is between raw cutting speed and the finished quality of the cut edge, which might require post-weld cleaning or finishing.
Gas Flow Management
When discussing plasma tools in general terms (like TIG welding), gas management becomes critical. For processes like Gas Tungsten Arc Welding (TIG), a protective shielding gas is used to surround the weld pool and prevent contamination from oxygen, nitrogen, and water vapor in the air, which could otherwise introduce defects or porosity into the final joint.
In TIG welding specifically, pure argon is often preferred as the primary shielding gas because it ensures stable arc characteristics. The required flow rate for this protective gas varies depending on the power source used; for example, when using a LNT 25 power source, the recommended argon shielding gas flow rate range is 10–15 liters per minute (L/min) as of 2025-11-25. Generally speaking, for TIG welding with argon, the typical shielding gas flow rate range falls between 10–35 cubic feet per hour (cfh), although this varies drastically from plasma cutting requirements.
It is important to distinguish that while some processes like TIG require precise control of noble gases like pure argon—supplied as high-purity welding-grade argon (around 99.99% or higher)—plasma cutting primarily uses the compressed air supply to create and sustain the plasma itself, making the pneumatic input the dominant gas consideration for portable units.
Selecting the Right Unit
Choosing a portable unit means weighing portability against required power density. You must assess the thickness of material you intend to cut most often—this dictates minimum amperage requirements. A machine rated for 40 A will handle specific pressures, requiring an input pressure range of 80–120 pounds per square inch (PSI) and supporting an air flow rate of approximately 5.3 cubic feet per minute (cfm).
For experienced operators moving between different metals or job sites, considering a unit with variable voltage control is beneficial. The ability to manage the electrical output within that core DC range of 200–400 volts allows for optimal arc stability regardless of minor changes in material thickness or ambient conditions.
Trade-off consideration: Units built purely for maximum portability may sacrifice robust gas and power inlet connections, while heavy-duty units might require significant setup time and specialized lifting equipment. Always ensure the unit's overall power consumption matches the available site electricity source (e.g., generators or dedicated circuits) to prevent brownouts that can cause arcing issues or unstable cuts.
Matching the compressor to the cutter, not the other way around
Size the air supply first and buy the plasma cutter second, because the cutter's spec sheet will tell you exactly what the compressor has to deliver and the reverse is not true. A 40 A air plasma cutter wants 80–120 PSI at the torch and pulls roughly 5.3 cfm while it does it. That flow figure is the one people miss. A small pancake or hot-dog compressor that tops out around a couple of cfm will hold pressure at the regulator while the machine is idle and then collapse the moment you pull the trigger, and the symptom is unmistakable: the arc starts fine, cuts cleanly for a second or two, then sputters, leaves a ragged dross-heavy kerf, and the cutter's fault light blinks. Operators blame the consumables and change the electrode, and it happens again on the next cut.
What you actually need is a compressor whose continuous delivery at your working pressure meets or beats the cutter's rated consumption, plus a tank big enough to ride out the surge when the arc strikes. A small tank and a marginal pump will cycle constantly and dump water into the line, and moisture is the other quiet killer—wet air erodes electrodes fast and produces porosity-looking pits along the cut face. Put a separator and a desiccant or coalescing filter within a few feet of the machine's air inlet, not back at the compressor, and drain the tank every session. If your only option is a compressor that just barely keeps up, shorten your cuts and let the tank recover between them rather than holding the trigger through a long rip.
This is the wrong approach when you're cutting thin sheet in short bursts all day—a smaller, cheaper compressor with a decent tank can keep up with that duty cycle fine, and spending on a huge pump is money you could put into a better torch. The honest trade-off is that a compressor sized for full duty on a 40 A machine costs more than many people expect and takes up real space in a truck bed.
Power supply, voltage, and what actually browns out
Check that your input power can carry the cutter's draw before you commit, because the arc itself needs a common DC voltage range of 200–400 volts DC to start and hold, and the machine's inverter has to produce that from whatever you feed it. On a dedicated 240 V circuit or a properly sized generator this is routine. On a long extension cord, a shared circuit, or an undersized generator, the input voltage sags under load and the symptoms show up as hard-starting, an arc that won't transfer to the work, or a cutter that trips its breaker mid-cut.
The practical sequence: run the shortest, heaviest-gauge cord you can, keep it off shared circuits, and if you're on a generator, size it for the cutter's starting surge rather than its running watts. Test the setup on scrap before you're standing over a part you care about. A machine that cuts cleanly on shop power and stutters in the field is almost always an input-supply problem, not a torch problem.
Variable output control earns its keep here. Being able to dial the current down for thin material keeps you inside that operating envelope instead of fighting an arc that's too hot for the gauge, and it lets you match the machine to a marginal power source rather than maxing it out on every cut. The cost is complexity and a few more settings to learn; the benefit is fewer blown consumables and cleaner edges on sheet. If you only ever cut one thickness of one material on good power, a fixed-output machine is cheaper and simpler and you won't miss the dial.
Consumables, duty cycle, and the cuts that tell you something's wrong
Buy consumables in sets and track how many cuts you get per electrode, because that number is your early-warning system for everything else on this list. A machine running dry, clean air at the right pressure and a stable input will run an electrode for a long, predictable stretch. The same machine on wet air or a sagging supply will eat electrodes noticeably faster, and the wear pattern tells you which: a gouged, off-center crater points to air problems, while erratic starting and short life across fresh consumables points to power. Keep a spare electrode, nozzle, and swirl ring on hand—running a worn nozzle "just a little longer" widens the kerf, throws dross, and can damage the torch head, which costs far more than the part you saved.
Watch the duty cycle honestly. Portable units are rated for a percentage of time at a given amperage, and the thermal cutout that stops you mid-cut is the machine protecting itself—not a defect. If you're regularly hitting it, you're either cutting thicker material than the machine is meant for or holding the trigger longer than the rating allows; back off to a lower current or break the work into shorter passes and let it cool. Piercing is the other heat trap: piercing thick plate at full power on a small machine is hard on nozzles, so start cuts from the edge where you can and save pierces for when you have to.
For the cut itself, keep a consistent standoff and travel speed and let the arc do the work rather than pushing the torch into the metal. A cut that's clean on top and heavily drossed on the bottom usually means you're moving too slow or running too much current; a cut with a beveled, ragged top edge usually means too fast or too little current. Read the kerf and adjust one variable at a time. The trade-off with all of this discipline is speed—chasing a perfect edge on every cut is slower than ripping through and grinding later, and for structural work where the edge gets cleaned up anyway, a slightly rougher cut at higher speed is the right call. Match the finish to the job instead of treating every cut like it's going on a showpiece.