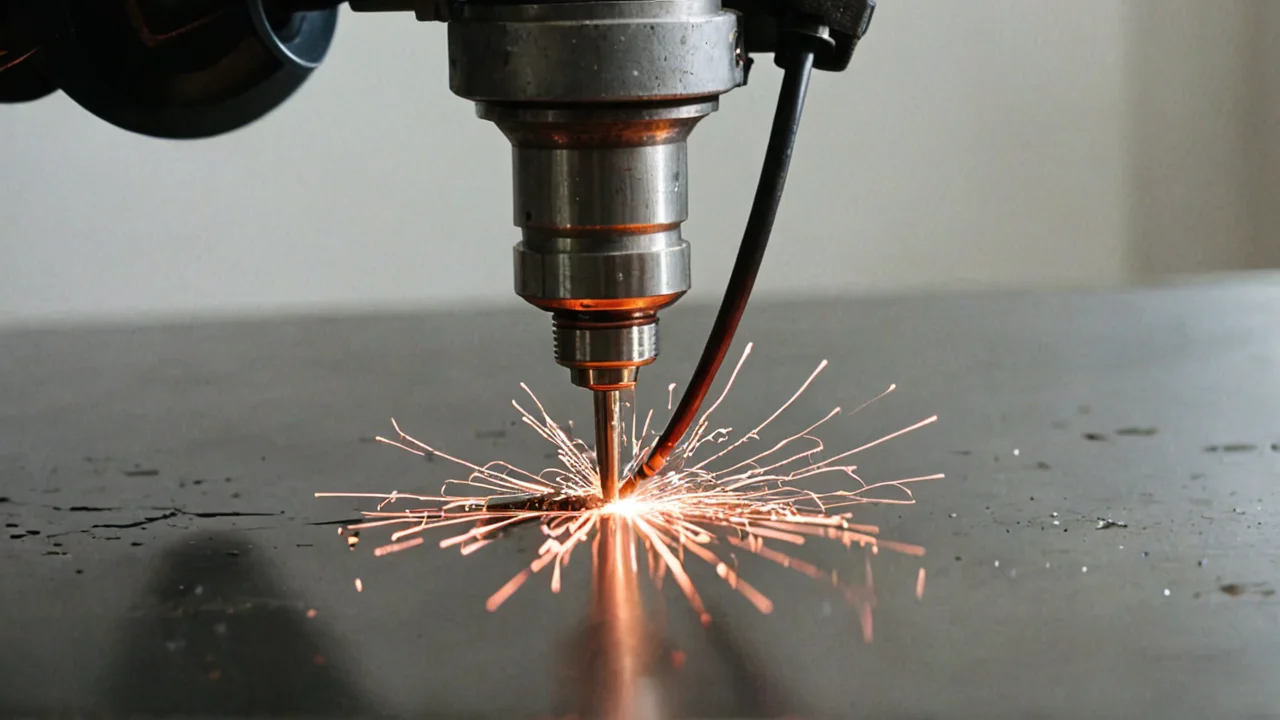
Before you even turn on the machine, ensure your personal protective equipment includes a certified face shield rated for intense arc light and appropriate leather gloves; improper PPE is the single greatest risk factor when working with plasma. The core mechanism relies on sustaining an electrical arc that superheats an inert gas into a highly conductive plasma stream capable of cutting through various materials.
What exactly is a plasma cutter?
A plasma cutter generates a high-velocity, superheated jet of electrically ionized gas—the plasma—by passing electricity through a restrictive orifice. It is essentially an advanced thermal cutting tool that utilizes electrical energy to achieve extremely high temperatures, allowing it to melt and blow away material rather than just charring or burning it.
The process begins when the machine applies voltage to create a stable arc across a constricted electrode tip. This intense electric current forces gas through the small opening, heating it instantly until it reaches plasma state—a mix of free electrons and ions. The properties of this plasma stream determine its cutting efficiency; generally speaking, higher amperage allows for greater heat transfer and deeper penetration into the workpiece.
You must understand that a plasma cutter is not simply a glorified blowtorch; its effectiveness comes from maintaining a controlled, high-energy arc over a precise opening. Because of this nature, while they are highly versatile, their operational parameters—including air pressure and voltage—must be precisely managed to achieve clean cuts.
How does the process work and what gas is needed?
The functionality of plasma cutting hinges on generating and maintaining an electrical arc using a specific shielding medium. For optimal performance, the cutter requires a regulated supply of compressed air. For instance, running a 40 A air plasma cutter demands a minimum input pressure range between 80–120 pounds per square inch (PSI), which supplies an approximate airflow rate of 5.3 cubic feet per minute (cfm). This combination of voltage and pressurized gas creates the cutting energy.
The electrical requirements are also critical, typically needing to maintain a common DC voltage range between 200–400 volts DC to reliably start and sustain the arc. It is crucial that this power source can handle sudden fluctuations in draw; otherwise, the arc will become unstable, leading to slag buildup or an uneven cut edge.
While plasma cutting primarily uses compressed air as its working gas—the medium that gets superheated into plasma—other specialized processes like TIG welding use inert shielding gases such as pure argon. This is a key difference: in TIG, the gas protects a weld pool from contamination; in plasma cutting, the gas is the cutting medium itself, providing the necessary conductive material to achieve thermal separation.
Can I cut aluminum or other metals with a plasma cutter?
Yes, plasma cutters are designed for use across several metal types, including common materials like steel and stainless steel. However, when dealing with highly conductive or reactive metals, you must adjust your machine's settings because the thermal properties of different alloys change how the plasma interacts with them.
When cutting aluminum, for example, proper setup is even more critical than with mild steel. Aluminum requires consistent voltage and a stable flow rate to prevent excessive warping and maintain kerf width. If you notice the cut edge becoming rough or excessively feathered, it usually means the machine is struggling to dissipate the heat rapidly enough through the material.
A general rule of thumb when considering trade-offs in materials is that thicker gauge metals will require significantly more stable voltage input and possibly higher pressures than thinner sheets. Always consult the equipment manual for specific amperage limits, as pushing a cutter beyond its recommended capacity, regardless of the material, increases the risk of electrical failure or unstable arc operation.
How should I set up and operate the machine safely?
Safety is not optional; it must be built into every step of the process. Before commencing work, always clear the immediate area of flammable liquids, dust buildup, or any materials that could ignite from stray sparks or plasma flare-ups. The act of cutting generates tremendous heat and intense UV/IR radiation.
Operationally, you must establish a stable working angle and feed rate. Plasma cutters are meant to be pulled through the material consistently; do not attempt to hold the torch stationary over an area while adjusting settings—this guarantees inconsistent results. Maintain adequate distance between yourself and the arc, allowing the plasma stream to perform its work without direct interference from your body or clothing.
Furthermore, because this process involves high voltage DC power, treat all cables and connections as live electrical components until you are certain they have been de-energized. Always secure gas regulators and air lines properly; a sudden failure or leak could lead to unexpected pressure releases or contaminated plasma operation.
What advanced techniques or limitations should I know?
While the basic function is straightforward, achieving high quality cuts often depends on understanding the nuances of arc management. One common limitation you will face is that plasma cutters are best suited for straight, uniform-thickness cuts; complex curves or intricate cut patterns require careful speed control to prevent inconsistent penetration.
When considering specialized processes, it's worth noting how different welding methods approach shielding gas. For instance, TIG welding utilizes a protective atmosphere—often 100% argon or an argon-helium mixture—to shield the molten pool from atmospheric contamination, preventing defects like porosity. This demonstrates that while plasma cutting uses air as its medium, other precision processes require controlled inert environments.
A trade-off to remember is between cut speed and edge quality: increasing your travel speed will increase throughput but usually decreases the cosmetic quality of the kerf (cut edge). For visible or critical joints where finish matters more than raw speed, you must slow down and maintain a highly consistent approach angle. Remember that every machine has limitations; if the material requires an amperage setting outside the standard operational range for your specific unit, switching to another cutting technology may be the responsible choice.
What actually goes wrong with the air supply, and how do you catch it before it ruins a cut?
Moisture and oil in the air line are the most common cause of a cut that looks like the machine is failing when it isn't. A 40 A air plasma cutter wants a regulated 80–120 PSI feeding roughly 5.3 cfm, and that spec assumes dry, clean air. A compressor that has been sitting, a tank with no auto-drain, or a run of hose laid on a cold floor will push water vapor into the torch, where it disrupts the arc, pits the electrode, and leaves a dross-heavy, ragged kerf. You notice it as a cut that starts clean on the lead-in and then wanders, or an electrode that dies well short of its expected life.
Fix the supply before you touch the machine settings. Put a coalescing filter and a desiccant or refrigerated dryer at the point of use, drain the compressor tank at the end of every session, and keep the last few feet of hose off the ground. If your air is marginal, run a test cut on scrap before every job that matters — a short straight pass on the same thickness you're about to cut tells you more in ten seconds than staring at the gauge does. The cost of a decent filter-dryer setup is small next to a box of electrodes and a ruined part.
Pressure itself is the other half. Too low and the arc won't transfer cleanly or will sputter mid-cut; too high and you get excessive dross and a wider, more angled kerf because the jet is blowing the molten metal sideways instead of down and out. Set pressure with the torch flowing, not static — a regulator that reads correctly with the trigger off will sag under flow. Watch the gauge during the cut, not before it.
How do you sequence a cut so the pierce doesn't wreck the part?
Pierce off the part, not on it. On anything thicker than sheet, start the arc with the torch angled so the pierce blows away from the finished edge, then rotate to perpendicular once the arc has punched through. Piercing straight down on a finished edge blows molten metal back over it and leaves a crater that no amount of dressing will hide on a visible joint.
Lead in from scrap or from the drop side, run the cut in one continuous pass, and lead out past the end of the part rather than stopping on the line. Stopping mid-cut is where you get the divot at the end of the kerf. On interior features — holes, slots — cut them first while the plate is still whole and supported, then cut the perimeter last, so the part doesn't shift or drop away and pinch the torch.
Consumable condition drives the sequence more than most operators admit. A worn electrode or a nozzle with an enlarged orifice changes the arc shape, and the cut quality falls off before the part visibly fails. Keep a spare set on the bench, swap when the cut starts showing a bevel on one side or dross that won't chip, and don't try to nurse a set through a job you care about. The machine will still cut; it just won't cut straight.
Grounding is part of the sequence too. Clamp the work lead to clean, bare metal on the part itself — not to the slatted table, not through paint or mill scale. A poor ground shows up as an arc that struggles to transfer, intermittently drops out, or cuts fine on one side of the plate and badly on the other. On a large sheet, move the clamp as you work around it rather than trusting one attachment point for the whole layout.
When is a plasma cutter the wrong tool, and what do you reach for instead?
Plasma is the wrong choice when you need a narrow, square, dimensionally tight kerf on thin material, or when the cut edge is a finished surface. The process removes material with a jet, so the kerf has a natural bevel and a heat-affected zone, and the edge usually needs dressing before it welds or assembles cleanly. For thin sheet where edge quality and tolerance matter, a shear, a nibbler, or a saw will give you a squarer edge with less cleanup, at the cost of being slower on complex profiles.
It's also the wrong tool when the power supply can't carry the load. The arc needs a common DC range of 200–400 volts DC to start and stay lit, and a circuit that browns out under that draw gives you an arc that starts, cuts for a moment, and drops — which reads as a torch problem but is a supply problem. Check the circuit and the extension cord before you blame the consumables. Long undersized cords are a frequent culprit; a dedicated circuit near the work is cheaper than chasing phantom faults.
There's a related distinction worth keeping straight if you also TIG. In TIG, the shielding gas — pure argon or an argon-helium mix — exists to keep oxygen, nitrogen, and water vapor off the molten pool, and the flow is set in a range of 10–35 cfh on typical equipment (10–15 L/min on an LNT 25 power source). In plasma cutting, the air is the cutting medium, not a shield, so treating the two processes as interchangeable on the gas side leads to bad settings on both. If you're running both machines in one shop, label the regulators and keep the argon and the shop air on separate drops so nobody sets a TIG flow rate on a plasma torch or the reverse. Arc-start method matters here too: lift TIG starting touches the tungsten to the work at low open-circuit voltage and lifts, which keeps high-frequency interference away from nearby electronics — worth knowing if your plasma table's control electronics sit close to a TIG setup.
The honest trade-off is this: plasma wins on speed, thickness range, and the ability to cut painted, rusty, or stacked material without setup. It loses on edge finish, kerf tolerance, and the amount of post-cut cleanup. If your job is a weldment where the cut edge gets ground and fitted anyway, plasma is almost always the right call. If the cut edge is the finished edge, budget the dressing time into the quote or choose a different process.