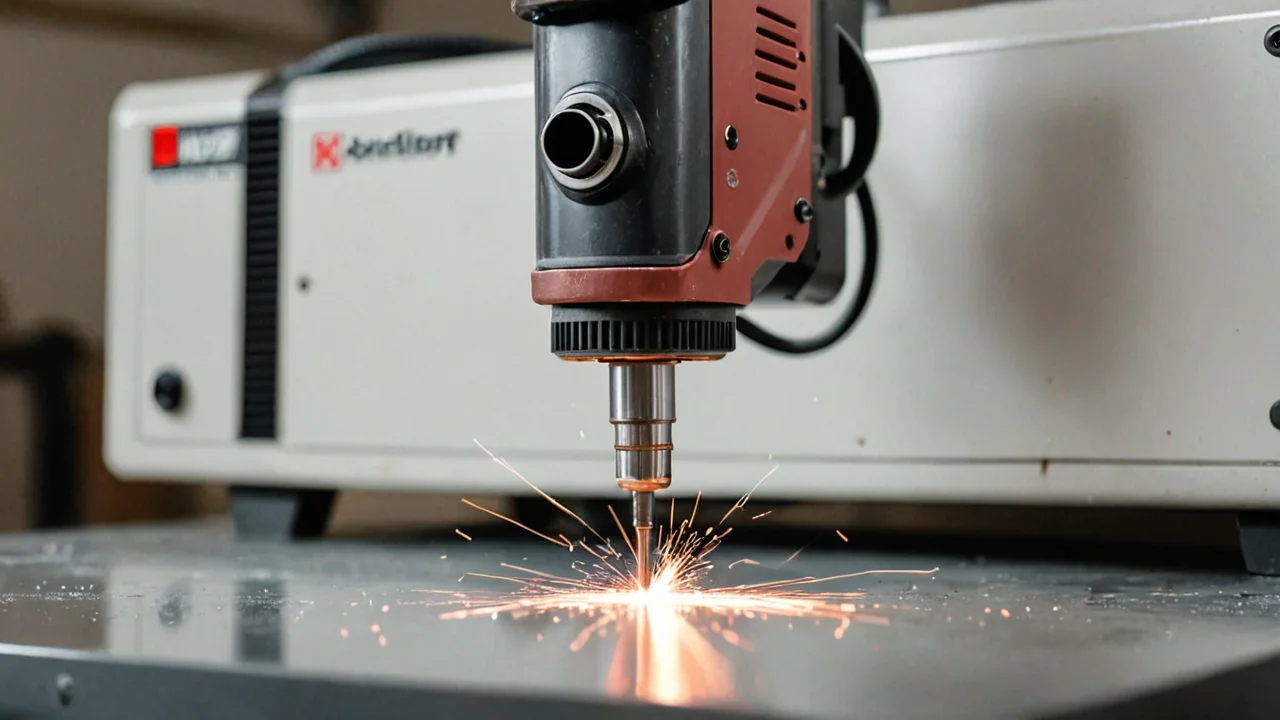
A plasma cutter generates an extremely hot, superheated stream of gas—the plasma arc—by passing high electrical current through a constricted gas stream; this focused heat is what rapidly melts and blows away metal. While modern hobby units have made these machines accessible, they are fundamentally different from simpler tools like angle grinders because the process relies on sustaining a precise voltage differential to create an ionized gas path.
Plasma cutting requires sufficient compressed air pressure and voltage to sustain its operating arc.
To use a plasma cutter effectively, you must ensure your system can provide both the necessary electrical potential and consistent airflow. The basic operation centers around maintaining a specific electric circuit: electricity is passed through a specialized torch head that constricts an inert gas (usually air or an air/gas mix) to form a stable arc. This process requires a common DC voltage range of 200–400 volts DC to start and maintain the plasma cutting arc.
The physical infrastructure needed for operation involves high-pressure air. For example, a 40 A air plasma cutter specifically needs a compressed air supply pressure range between 80–120 pounds per square inch (PSI). At this specified pressure, the machine delivers an approximate air flow rate of 5.3 cubic feet per minute (cfm), which is crucial for keeping the arc focused and stable across different materials.
The primary drawback here—and it’s a major trade-off to be aware of—is that plasma cutting is not merely "burning" metal; it's an aggressive, thermal material removal process. This means you are dealing with intense heat and flying debris, which demands strict adherence to safety protocols, including specialized shielding and appropriate Personal Protective Equipment (PPE). You cannot treat this like simple sheet metal trimming.
Plasma cutters excel at cutting many conductive metals but lack the precision of dedicated welding processes.
When considering material compatibility, plasma cutters are highly versatile for hobbyist work on various common metals because they rely on heat transfer to melt and blow through the material. The process works by turning a gas into plasma—an electrically charged state that is incredibly hot. When this superheated stream hits conductive metal, it rapidly heats the target area until its melting point is reached, at which point the kinetic force of the high-velocity gas blows the molten metal away.
While you can certainly cut aluminum with a plasma cutter, remember that while some welding processes like TIG are commonly used for precise, high‑quality welds on metals such as steel, stainless steel, and aluminum, these alternative methods offer different trade-offs. Plasma is fast but inherently rougher than controlled arc processes.
If your goal is purely aesthetic, flawless seams—say, when working with a pure argon shielding gas for TIG welding to prevent contamination of the weld pool—then plasma cutting is often overkill and too aggressive. However, if you need to cut through thick sections quickly on site where speed outweighs absolute surface finish, plasma remains an industry workhorse.
Achieving high-quality results requires treating plasma cutting as a specialized thermal removal process rather than a simple arc weld.
Operating a plasma cutter is straightforward in theory—set the machine to the correct amperage and apply the torch—but mastering it takes experience because you are managing immense amounts of energy. The key difference between plasma cutting and other processes, like Gas Tungsten Arc Welding (GTAW) or TIG welding, lies in the objective: Plasma removes material; TIG joins material. You must treat them as distinct skills.
Unlike TIG welding, which requires a carefully managed inert shielding gas—most commonly 100% argon or argon‑helium mixtures—and involves precise flow rate management (for example, a recommended argon shielding gas flow rate for LNT 25 power source is 10–15 liters per minute), the plasma cutter uses its inherent air pressure and electrical potential to do the heavy lifting. You are not protecting a weld pool; you are blowing away molten metal.
A significant operational limitation, however, is that plasma cutting requires constant attention to the feed rate of your gas supply. If the compressed air drops below 80–120 pounds per square inch (PSI), the torch will lose its stability and arc consistency, leading to a ragged cut edge or even an immediate outage. It’s a trade-off: maximum speed comes at the cost of high energy demands on your air compressor system.
Plasma cutting is best suited for quick removal cuts where material thickness is consistent; it should not replace delicate joining methods.
The ultimate utility of the plasma cutter is defined by what you are willing to sacrifice: time, precision, and surface finish. When compared to dedicated welding processes like TIG, which use a nonconsumable tungsten electrode and an inert shielding gas (like pure argon, supplied typically as high‑purity welding‑grade argon around 99.99% or higher), plasma is faster but much rougher.
When you look at the mechanics of joining metal—the TIG process uses a protective gas directed around the tungsten electrode and weld pool to prevent contact with atmospheric contamination, which can cause porosity and weld defects—you realize that joining requires careful chemical control. Plasma cutting bypasses this chemistry; it is purely mechanical removal driven by heat and force.
If your project demands a flawless joint that will undergo stress or high temperature cycling later in life, you should be using TIG welding (GTAW). If the job is simply "remove this piece of metal quickly," plasma excels. The major trade-off to remember is that while argon shielding gas flow rates for TIG might range from 10–35 cubic feet per hour (cfh), a plasma cutter’s performance relies on maintaining high, stable air pressure and the correct DC voltage (200–400 volts DC) rather than complex gas mixtures.
Your compressor is the real limit on cut quality, not the cutter's amperage rating
Before you blame the torch for a ragged edge or a cut that won't fully sever, check the gauge at the machine's air inlet while the arc is running. A 40 A air plasma cutter wants 80–120 PSI at the torch and pulls roughly 5.3 cfm at that pressure. Most small hobby compressors are rated on a free-air displacement number that has nothing to do with what they deliver continuously, and the number that matters is the one printed next to a pressure rating — the cfm the pump can hold while the tank is refilling, not the peak. A compressor that can't sustain the flow will let pressure sag the moment the arc fires, and the symptom is specific: the cut starts clean, then the kerf widens and drosses up a few inches in as the pressure falls. You'll hear the motor kick on and stay on.
Two fixes cost almost nothing. First, add a dedicated air/water separator and filter right at the cutter's inlet — plasma air needs to be dry, and a wet tank pushes moisture into the torch, which shortens consumable life and produces erratic arcs. Second, set the regulator with the machine running and cutting, not static, so you're reading working pressure rather than tank pressure. If your compressor still can't hold the band, the honest answer is a larger tank or a bigger pump; turning the amperage down to compensate just gives you a slow, cold cut with more dross, not a better one. The trade-off of a small hobby cutter is real: it is only as good as the air behind it.
Watch the consumables as your first diagnostic. A worn electrode and nozzle show up as a cut that won't stay perpendicular, a kerf that wanders, or a pilot arc that struggles to transfer to the work. Change them as a set, not one at a time, and keep the shield cup clean — spatter bridging the nozzle orifice is the most common cause of a cut that suddenly goes bad mid-job.
Set the machine in this order, and don't touch amperage to fix a travel-speed problem
Get your sequence right and most of the guesswork disappears. Start with clean, dry air verified at working pressure. Then set amperage to the material thickness per the cut chart on the machine or in the manual — not higher "to be safe." Then set your standoff and drag or pierce height per the torch's shield design. Only after those are fixed do you adjust travel speed, and travel speed is the variable you should be changing most often. Too fast leaves an unsevered bottom edge and a backward-angled kerf; too slow piles up dross and overheats the nozzle.
The mistake almost everyone makes early on is cranking amperage to force a cut through material the machine is rated to handle only marginally. That buys you a hotter, wider kerf, faster consumable wear, and a nastier edge — it does not buy a cleaner cut. The other common error is piercing thick plate at full power with the torch held at drag height; pierce at a standoff, let the arc blow through, then drop to cut height and move. Piercing at contact height blows molten metal back into the nozzle.
Grounding deserves its own minute. A poor work clamp connection — clamped to paint, rust, or a coated surface — causes erratic arc transfer and hard starting, and it's easy to mistake for a torch fault. Clamp to bare, clean metal close to the cut, and check the clamp jaw for corrosion. On thinner gauge sheet, a drag tip and a straightedge guide will do more for edge quality than any setting change, because hand travel on thin material is where the wobble comes from.
Know where plasma stops being the right tool and a saw or a TIG torch takes over
Plasma is a removal process, and it leaves a heat-affected zone and a slightly tapered kerf that you will have to dress. If the part needs a machined edge, a square shoulder, or a weld-ready fit-up with tight gap control, cut it oversize with plasma and finish it — or choose a saw or shear for straight cuts in thin sheet and let plasma handle curves, holes, and demolition work where its speed wins. That division of labor is the practical answer to "when do I not use this."
The comparison to TIG matters here because the two processes get confused by beginners shopping for one machine. TIG joins metal with a nonconsumable tungsten electrode under an inert shield — most commonly 100% argon or argon-helium — and the gas flow is a controlled, modest setting, on the order of 10–35 cfh on general argon work and 10–15 L/min on a source like the LNT 25. That gas is there to keep oxygen, nitrogen, and water vapor off the molten pool; get it wrong and you get porosity, not a bad cut. Plasma has no weld pool to protect — its air is the cutting medium, and the failure mode is a ragged kerf, not a contaminated joint. If you plan to start TIG arcs on the same bench, note that lift-arc starting (touch and lift at low open-circuit voltage) avoids the high-frequency interference that can upset nearby electronics in a small shop.
Budget for consumables and air as part of the cost of ownership, not an afterthought. Nozzles, electrodes, and shields wear on a schedule tied to how much you pierce and how clean your air is; a dry-air setup stretches that schedule noticeably, and a wet one shortens it. The DC voltage the machine needs to strike and hold the arc — in the 200–400 VDC range — is handled inside the box, so your job is the air, the ground, the consumables, and your hand speed. Get those four right and a hobby cutter will cut cleanly through the metals it's rated for; fight them and no amount of amperage will save the edge.
Drag tips versus standoff: match the shield to the cut, not the other way around
Use a drag shield whenever the material is thin enough that hand wobble is your biggest error source, and switch to a standoff shield only when you need to pierce or when the torch's own design calls for it. A drag tip rides directly on the plate, which fixes your standoff at a constant height and removes one variable from the cut — on gauge sheet that alone cleans up the edge more than any amperage tweak. The cost is that dragging generates friction and heat at the shield, and on long cuts the tip wears faster; you'll notice it as a cut that starts fine and then begins to wander or lose the arc on the back half.
Standoff shields keep the nozzle off the work, which is what you want for piercing thick plate and for cutting over slats or expanded material where there's nothing solid to ride on. The trade-off is that you now own the height by hand, and inconsistent height shows up as a kerf that varies in width down its length. If you're seeing that, the fix is a guide or a fence, not a new torch. Check the shield cup before every session: spatter bridging the nozzle orifice is the most common reason a cut that was clean yesterday goes ragged today, and it's a two-minute swap.
Cutting over water, slats, and rusty plate: the cases the manual skips
Cutting over a water table or in a tray changes your air demand in a way that's easy to miss — the arc now has to push molten metal and vapor out of a wet kerf, and a marginal air supply that held pressure on dry plate will sag here. Verify working pressure at the inlet with the arc running, not static, and don't be surprised if you have to slow travel to keep the bottom edge severed. The upside is less dross sticking to the underside and cooler parts; the downside is more smoke off the surface and a splash hazard you should plan PPE around.
Rust, mill scale, and paint are where hobby cutters get blamed unfairly. The arc has to establish through the contamination, so you get hard starting and erratic transfer — the same symptoms as a bad work clamp. Clean a spot for the ground clamp to bare metal near the cut, and if the plate is heavily scaled, score the cut line or start from a drilled pierce point rather than forcing the arc through. On expanded metal and grating there's no continuous surface to drag on, so treat it as a standoff job and expect to sacrifice edge quality for getting through it at all.
The honest limit: none of this makes a hobby cutter a fabrication tool. If the part needs a square, weld-ready edge, cut it oversize and finish it on a saw or mill. Plasma earns its place on curves, holes, demolition, and anything where speed beats finish — and on those jobs, dry air, a clean ground, fresh consumables, and steady hand speed are the whole game.