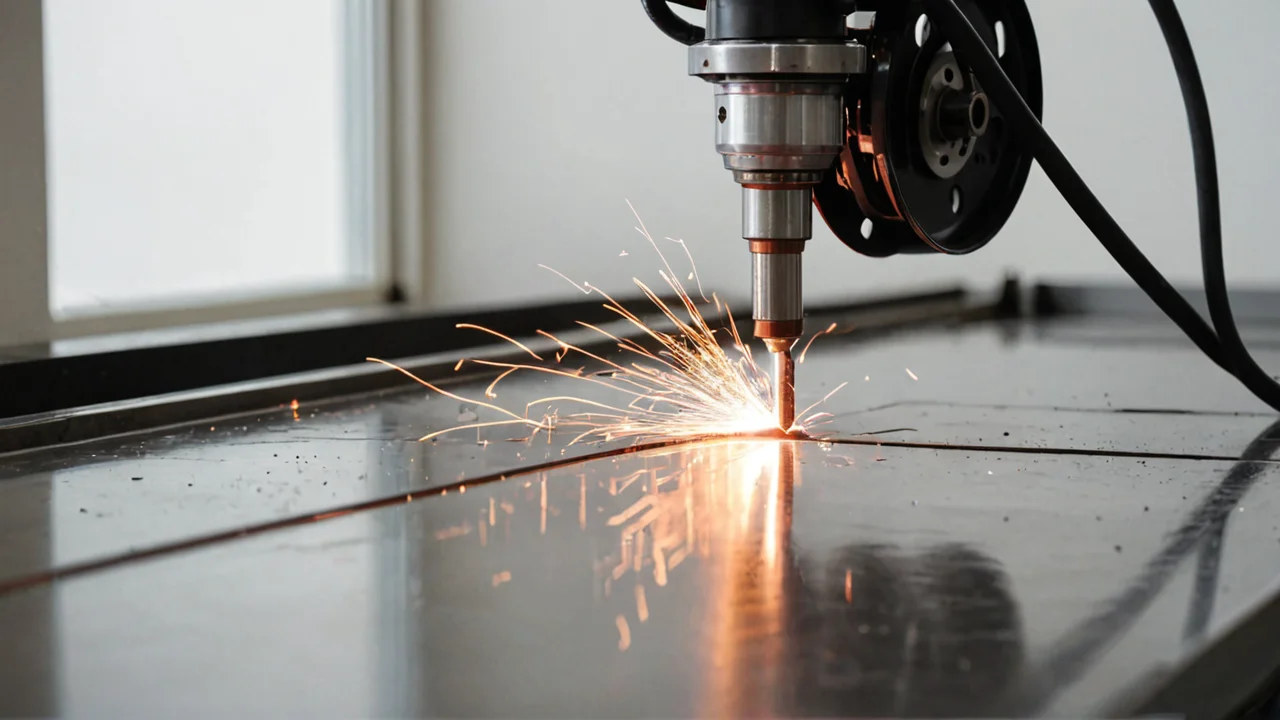
"Does a plasma cutter actually cut aluminum?" The answer is yes, but success depends heavily on knowing the correct machine settings and managing the thermal stresses inherent to the material.
Plasma Arc Mechanism
A plasma cutting system does not use a chemical reaction; it uses extreme heat generated by an electrical arc passing through a highly pressurized gas stream. This process converts a basic gas—typically compressed air or oxygen mixed with other gases—into a superheated, electrically conductive state: plasma. The core function relies on establishing and maintaining the initial electric circuit.
To achieve this, the machine first requires high-pressure mechanical support. For instance, running a 40 A air plasma cutter demands a compressed air supply operating within an 80–120 pounds per square inch (PSI) range. This pressurized gas stream is then directed through a narrow nozzle and focused onto the workpiece. At the same time, the system applies electrical energy to create the arc itself. The necessary DC voltage range required to start and maintain this plasma cutting arc sits between 200–400 volts DC.
When these elements combine, the gas is superheated rapidly—reaching temperatures of thousands of degrees Fahrenheit—and becomes ionized (the definition of plasma). This focused, intensely hot stream of gas acts like a precision thermal torch. It heats the metal along its path until it reaches its critical vaporization temperature, creating an extremely localized molten zone and allowing the machine to cut cleanly through the material.
The power source controls both the voltage (which governs arc energy) and the air flow rate. At the specified pressure range, this plasma cutter generates an approximate air flow rate of 5.3 cubic feet per minute (cfm). Understanding that the process is fundamentally about controlled gas expansion under immense electrical stress helps differentiate it from slower thermal processes like oxy-fuel cutting.
Material Cutting Capabilities
Plasma cutters are remarkably versatile, handling everything from mild steel to specialized alloys, but their effectiveness changes dramatically when dealing with aluminum. While the machine itself can cut aluminum—and many professional shops do it daily—the trade-off is that you must manage high heat transfer and dross formation.
For basic metals like carbon steel or thick stainless steel, the plasma arc excels at rapid removal of material due to its sheer energy density. However, when cutting aluminum, which has a lower melting point than many ferrous metals and reacts more readily with atmospheric contaminants, you must be particularly mindful of machine settings. Aluminum requires careful control over gas composition; using pure oxygen or high-pressure air is critical, but the specific shielding requirements differ from standard steel cuts.
In fact, some plasma cutting systems are better suited for materials that require minimal clean-up compared to others. When working on aluminum, you will see a rapid vaporization of the material, which often generates oxide residue (dross). A key operational consideration is ensuring your gas supply and flow rate can maintain stability while managing this high volume of particulate waste.
Operational Setup
Operating a plasma cutter involves setting up three interconnected systems: the power source, the compressed air supply, and the consumables. You cannot simply point it at metal; the machine needs to be configured correctly for the specific job size and thickness.
Before you even touch the material, you need to confirm your gas pressures and flow rates are within spec. If using a standard 40 A air plasma cutter, remember that maintaining the required 80–120 pounds per square inch (PSI) supply pressure is non-negotiable for proper performance. Furthermore, the actual operational technique involves setting the machine so that the torch travels perpendicular to the cut line at a consistent speed.
The biggest mistake novice users make is treating it like a simple welding process. It isn't; the plasma cutter needs constant movement and careful angle management. The gas flow rate, which dictates how much material the plasma stream can carry away from the kerf (the cut path), must be optimized. While I recommend reading the specific manual for your setup, understanding that the electrical arc is what drives the cutting action, and the compressed air/gas simply feeds and directs it, is key to smooth operation.
Plasma vs. Arc Welding
It’s easy to confuse plasma cutting with traditional welding methods like TIG or MIG, but they are fundamentally different processes serving different purposes. Plasma cutting is a bulk material removal process; welding is an additive joining process.
Consider the difference: If you need to cut through 1/2 inch of steel quickly, plasma is ideal. If you need to join two pieces of aluminum together with maximum structural integrity while minimizing heat input and contamination risk, TIG (Gas Tungsten Arc Welding) is the superior choice.
This difference in application means that a trade-off decision must always be made before starting work. Plasma cutters are generally faster for through-cutting thick materials but leave a rougher edge and require post-weld clean-up due to the thermal damage caused by the intense heat. Conversely, TIG welding, which uses a nonconsumable tungsten electrode and an inert shielding gas like pure argon (often supplied at high‑purity welding‑grade argon around 99.99% or higher), provides incredibly precise welds but is slower.
Therefore, if the goal is simply to separate two pieces of metal quickly—and you don't need a pristine edge for structural joining—plasma cutting is fine. If the job requires minimal heat distortion and maximum quality in the joint itself, then you must switch processes entirely. The plasma cutter should never be used as a replacement for a proper arc welding process when high metallurgical integrity is required.
Consumable Stack Life and Failure Signals
The electrode and nozzle are the parts that die first, and they die in ways that tell you what you're doing wrong. The electrode is a copper body with a hafnium or tungsten insert at the tip; the arc burns from that insert, and once the insert is cratered deep enough the arc starts wandering and the cut edge goes ragged before the machine ever gives you a fault code. The nozzle is the constriction that shapes the plasma, and its orifice erodes from both the arc and the molten metal blowing back up through the kerf. When a cut that used to be clean starts leaving a bevel on one side only, or the arc won't transfer without a scratch start, you're usually past the point where the consumables should have been replaced.
What kills them early, in rough order of how often I see it:
- Piercing on thick plate with the torch down. The blowback of molten metal slams straight into the nozzle. Pierce at a standoff, or start the cut from the edge, and nozzle life roughly doubles on anything heavy.
- Moisture in the air line. A plasma torch runs on ionized gas, and water vapor in the supply disrupts that arc and eats electrodes. An inline coalescing filter and a desiccant dryer are cheap next to a box of electrodes.
- Cutting at the wrong amperage. Too much current for the thickness sets you up for faster consumption; too little gives you a slow, dross-heavy cut where the arc sputters and the nozzle takes the punishment instead of the workpiece.
- Wrong shield or swirl ring. Consumables are matched sets. Mixing a nozzle rated for one amperage with an electrode rated for another is the most common cause of a torch that "just won't cut straight anymore."
Torch height is the setting most people get wrong and the one with the clearest feedback. Drag cutting—torch riding directly on the plate—is fine on thin material and gives you a clean, tight kerf. On thicker plate, drag cutting overheats the nozzle and blows the kerf wide. A machine torch on a table with a height control keeps the standoff constant and is what separates a clean cut from a beveled one at thickness. The trade-off is real: hand drag cutting is faster to set up and needs no height control, but it costs you consumables and edge quality on anything but sheet.
Air Supply Quality: The Failure Almost Nobody Checks First
Before you touch amperage or torch speed, check the air. A plasma cutter specified for an 80–120 PSI supply and roughly 5.3 cfm at that pressure will cut poorly—or not at all—if the compressor can't hold that pressure while the arc is running. The number on the gauge when the machine is idle is meaningless. Watch the pressure while you're mid-cut: if it sags below the spec range, the arc loses its rigidity, the cut gets drossy, and you'll blame the consumables when the real problem is a small compressor cycling on and off.
This is the classic hobbyist failure. A small pancake compressor rated for a burst of air looks fine on paper but can't sustain the flow a plasma torch pulls for a long cut. The symptom is a cut that starts clean and then goes ragged as the air pressure drops, or a machine that fault-codes mid-cut on a long pass. The fix is either a larger tank and pump or a dedicated air supply, not a new torch.
Moisture is the other half of it. Compressed air carries water vapor out of the tank, and it condenses as the air expands through the torch. That water shows up as a sputtering arc, a rough cut edge, and electrodes that die young. A refrigerated dryer is the gold standard; a desiccant filter is the practical middle ground for a small shop. Drain the tank regularly and put a filter right at the machine inlet, not back at the compressor—the line between them collects its own water.
Gas choice for the cut itself matters too. Compressed air is the default for a 40 A class machine because it's cheap and works on mild steel and aluminum. Oxygen gives a faster, cleaner cut on carbon steel but is wrong for aluminum and stainless, where it oxidizes the cut face. Nitrogen is the choice for stainless where you want a clean, weldable edge without an oxide layer to grind off. The trade-off is cost and the need for a second gas bottle and regulator; for most shop work the air supply is fine, but if you're cutting stainless that goes straight to a weld, running air will cost you a grinding step on every part.
Where Plasma Stops and TIG Begins: The Shared Setup Discipline
The two processes share more setup discipline than people expect, and that's where the crossover jobs go wrong. If a plasma-cut edge is going straight into a TIG weld, the cut edge is the joint preparation, and the oxide and dross left on it will contaminate the weld pool. On stainless and aluminum that means grinding or at least wire-brushing the cut face before you strike an arc, because TIG with pure argon shielding—typically supplied as high-purity welding-grade argon around 99.99% or higher—will pull that contamination straight into the puddle and leave you with porosity you can't weld out.
The shielding gas setup on the TIG side follows its own numbers, and getting them wrong mirrors the plasma air-supply problem. Argon flow for TIG typically runs 10–35 cubic feet per hour on a general machine, and on a specific power source like the LNT 25 the recommended range is 10–15 liters per minute. Too little flow and the pool sees air; too much and the gas stream goes turbulent and pulls atmosphere in anyway, which is the counterintuitive failure that catches people who think "more shielding is safer." Set it to the machine's range, not to a guess.
Arc starting is the other crossover point worth knowing. TIG can start with high-frequency, which is easy but throws electromagnetic interference into nearby electronics, or with lift TIG, where you touch the tungsten to the work at low open-circuit voltage and lift to strike. Lift start is the safer choice near sensitive equipment and the one I'd reach for in a shop with a CNC table or a plasma cutter sharing the same circuit—high-frequency noise and a plasma power supply don't play well together, and the interference shows up as a fault on the other machine, not the one you're holding.
The honest trade-off: plasma is the right tool for separating metal, and TIG is the right tool for joining it with quality. A plasma cutter that's dialed in for a clean cut and a TIG torch set to its rated gas flow and a lift start will handle a cut-and-weld job from one bench. Skipping the edge prep or guessing at gas flow is where a job that looked simple turns into a porosity hunt. Neither process is a substitute for the other, and the shops that do both well are the ones that treat setup numbers—pressure, flow, standoff, current—as the actual work, not the paperwork before it.