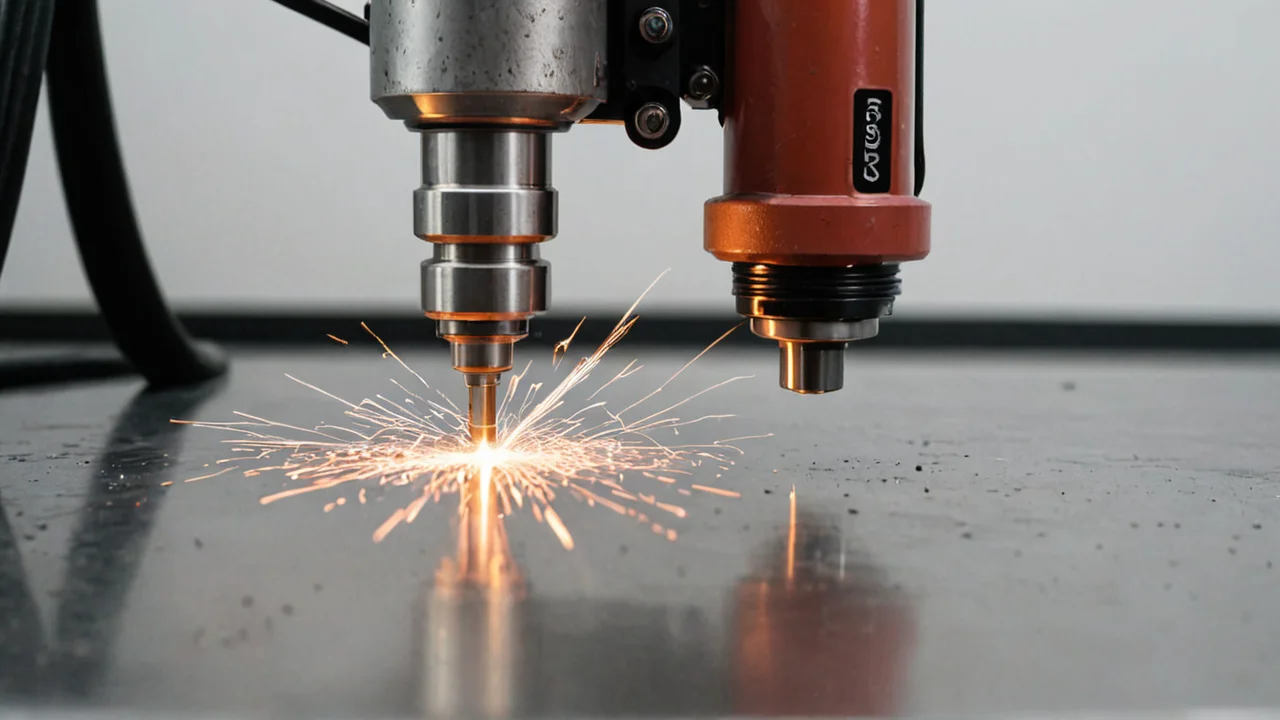
While the fundamental physics of plasma cutting—using an electrical arc superheated through an inert gas stream—remain unchanged, modern CNC setups have dramatically shifted from manual jigging and oxy-fuel methods to highly automated, high-precision processes capable of handling diverse materials like aluminum with minimal setup time.
Plasma Arc Fundamentals
At its core, a plasma cutter generates an electric arc that superheats an inert gas—most often compressed air or sometimes nitrogen—into a state called plasma. This process requires electricity to maintain the necessary voltage and pressure; specifically, common DC voltage ranges required to start and maintain this cutting arc fall between 200–400 volts DC.
The system works by forcing highly pressurized gas through a constricted nozzle (the torch). The electrical energy ionizes the gas, creating an extremely hot, high-velocity stream. This superheated plasma rapidly melts and expels the material it passes through. When discussing how to operate or use a plasma cutter generally, understanding that it fundamentally relies on this combination of intense heat and focused pressure is key. It’s not simply burning; it's controlled thermal erosion.
When you acquire a modern setup, remember that the machine must be correctly supplied with compressed air. For instance, a 40 A air plasma cutter requires a compressed air supply pressure range of 80–120 pounds per square inch (PSI), which translates to an approximate airflow rate of 5.3 cubic feet per minute (cfm). This pressurized gas is what carries the energy and ensures consistent cutting action.
Material Versatility
A common question when people first approach plasma cutting is whether it can cut aluminum, and the short answer is yes; plasma cutters are widely used for this purpose. However, you must understand that while they can cut it, other processes may offer superior finishes or cost savings depending on the thickness and required precision.
Plasma cutters operate by cutting through virtually any conductive metal material—steel, stainless steel, and aluminum included. The primary limiting factor is not usually the material type itself, but rather managing the heat transfer rate and controlling potential warping in thinner gauge metals. While the process can handle aluminum, achieving a clean cut on highly reflective or sensitive materials often requires careful management of the cutting speed and gas flow.
If you are planning to cut non-ferrous metals like aluminum frequently, keep in mind that while plasma is effective, it introduces significant heat into the surrounding area. For exceptionally high quality work where minimal thermal distortion is mandatory, a waterjet might be considered, but for general industrial throughput and thickness ranges, modern plasma cutters remain a robust choice.
CNC System Integration
The primary advantage of pairing a plasma cutter with CNC technology is moving the process from skilled manual labor to repeatable, precise automation. Where older setups required operators to interpret blueprints and manually guide the torch along marked lines—a slow, inconsistent process prone to human error—the CNC system takes over the entire pathing operation.
The machine integrates a digital controller that interprets CAD/CAM files, translating complex vector paths into precise X, Y, and Z axis movements. The operator's job shifts from physically guiding the torch to programming the toolpath and ensuring mechanical alignment. This repeatability is why plasma cutting on CNC equipment has become such an industrial standard for large-scale fabrication.
Implementing a CNC setup requires attention to fixture design. You must consider how your workpieces will be clamped and presented to the gantry or rail system. The machine needs to maintain consistent height (Z-axis) as it follows the path, which is especially critical when cutting curved geometries or intricate internal shapes.
Optimal Operational Parameters
Successful plasma cutting demands more than just powering on a unit; it requires dialing in specific operational parameters based on the material and thickness being cut. These settings determine efficiency, speed, and the quality of the final edge finish.
- Amperage/Voltage: The electrical settings must be appropriate for the desired cutting speed. While the initial arc voltage falls within the 200–400 volts DC range, the amperage controls the energy density applied to the metal.
- Gas Selection and Flow Rate: Although plasma cutters often use compressed air, some high-end setups may utilize other gases depending on the material. The proper gas flow is crucial for flushing molten metal slag away from the cutting zone as it passes through. Insufficient flushing leads to "dross" buildup, which ruins the cut edge finish and can cause localized overheating or erratic cuts.
- Torch Speed: This controls the rate at which the plasma stream traverses the material. Too fast, and you don't achieve full penetration; too slow, and the heat input causes excessive warping and burn-through.
When operating a CNC setup, these parameters are often managed by the machine controller itself, allowing for dynamic adjustments mid-job—for instance, slightly increasing flow rate when encountering thicker sections of steel compared to thinner gauge aluminum.
Trade-offs and Limitations
While incredibly versatile, plasma cutting is not always the best tool for every job. Understanding its limitations prevents costly rework down the line.
The most significant trade-off is the inherent heat input. Because the process involves superheating a gas stream to melt metal, there will always be a Heat Affected Zone (HAZ) around the cut path. This can compromise the metallurgical properties of the material immediately adjacent to the plasma line. For critical structural welds or components that require maximum strength retention near the edge, this HAZ must be factored into your design tolerances.
Another consideration is cleanup. Plasma cutting produces significant amounts of oxidized residue (dross). While modern machines are designed to minimize spatter and slag buildup, the resulting cut edges will need subsequent finishing—grinding or chemical treatment—if a perfect, pristine edge profile is required for final assembly. It is far cheaper in the long run to budget time and material for this post-processing step than it is to deal with structural failure due to edge integrity issues.
Advanced Techniques
High-end industrial applications often integrate plasma cutting with other processes, such as grinding or laser profiling, to mitigate its inherent thermal weaknesses. For example, a setup might use the CNC coordinates not just for the cut itself, but also to guide an auxiliary grinder head immediately following the pass, effectively removing the accumulated dross and smoothing the HAZ.
Some highly specialized systems are beginning to incorporate gas monitoring and feedback loops directly into the CNC programming. These advanced controls constantly analyze the plasma stream characteristics—such as current draw fluctuations or pressure drops—and adjust the voltage or flow rate in real-time, ensuring that the cutting process remains perfectly stable regardless of minor variations in material composition or thickness encountered mid-run.
Mastering this technology means understanding both the physics (the high voltages and PSI requirements) and the digital control layer. It’s a blend of classical metallurgy meeting modern computerized automation.
Air Supply: The Failure Point Nobody Budgets For
Specify the compressor and dryer before you specify the table, because a CNC plasma will run the torch harder and longer than a manual operator ever did. A 40 A air plasma cutter wants a compressed air supply pressure range of 80–120 PSI at roughly 5.3 cfm, and it wants that continuously for the length of a nesting run—not in the bursts a hand cutter sees. A small reciprocating compressor with a modest tank will cycle constantly and drag its pressure down mid-cut, and the symptom shows up as a ragged kerf on the second or third part of a nest while the first part looked perfect. You will chase torch consumables for a week before you suspect the air.
Put a refrigerated dryer and a coalescing filter ahead of the machine's inlet, and drain the tank and bowl on a schedule you actually keep. Moisture in the plasma gas shows up as porosity-like pitting on the cut face, uneven dross that sticks hard rather than flaking, and consumable life that varies wildly from one electrode to the next. The torch itself will tell you: a nozzle that erodes off-center means something upstream is dirty or the flow is unstable.
Size the compressor for duty cycle, not for peak cfm. Cutting thin gauge at high speed is a near-continuous demand, and a compressor rated at the right cfm but a low duty cycle will overheat by mid-afternoon. If your shop air is shared with other equipment, give the plasma table its own drop and its own regulator at the machine. The cost is a compressor with real headroom, a dryer, and a filter—cheaper than the labor of diagnosing a defect that only appears on long jobs.
Setting the Cut Chart and Torch Height Before the First Part
Build your own cut chart before you trust the one in the manual, because the published numbers assume a specific torch, a specific consumable stack, and clean, dry air at the right pressure. Start with the manufacturer's recommended amperage, feed rate, and pierce height for the material and thickness, run a test coupon, then adjust one variable at a time. If the dross is heavy and fused to the bottom edge, you are usually too slow or running too much amperage for the thickness; if the kerf has a pronounced bevel on one side and the arc lags behind the travel, you are too fast. Change feed rate first, then amperage, then height. Never touch all three in the same test.
Torch height control matters more on a CNC than it ever did by hand. The arc voltage feedback loop keeps the nozzle at a consistent standoff, which is what makes the kerf width repeatable across a long path. Set the pierce height higher than the cut height and program a delay before the machine starts moving, or you will blow the nozzle on thick plate. On thin gauge, keep the pierce short and start the lead-in off the finished edge so the pierce divot lands in scrap. The voltage you are working with is substantial—common DC voltage ranges to start and maintain the cutting arc fall between 200–400 volts DC—so treat the torch lead and work clamp as a circuit, not an accessory. A poor work clamp connection shows up as erratic arc starting and inconsistent cut quality that moves around the table as the clamp heats up.
Cut a test coupon on every material and thickness you run, keep the settings written down, and re-verify after every consumable change. The cost of this discipline is scrap plate and an hour of setup; the cost of skipping it is a nest of parts that all need rework.
Nesting, Lead-ins, and the Sequence That Saves the Plate
Program the cut sequence so each part is fully cut before the torch moves to the next, and so the machine never crosses a previously cut kerf at speed. Cutting a part free while its neighbor is still attached lets the freed piece shift and tip into the torch path—one of the most common causes of a crashed nozzle and a ruined plate. Nest with enough web between parts for the kerf plus the heat-affected zone, and put the pierce point in scrap, not on the finished edge.
On thin material, sequence matters for a second reason: heat. Consecutive cuts in the same region stack heat into the plate and the warping compounds, so spread the cuts across the sheet and let the geometry cool between passes. If the plate starts to bow, you will see the torch height control fighting to hold standoff and the kerf widening on one side. The fix is a better nest and a slower overall program, not a different consumable.
Finally, decouple the plasma from the rest of the shop. The high-frequency start and the arc itself are noisy, and the arc voltage loop is sensitive to a bad ground. Run the work clamp directly to the plate, keep the table ground separate from the building steel where you can, and route the torch lead away from the controller cabling. When the machine drops the arc on the same corner of every part, the problem is almost always the ground path or the lead routing, not the torch. Get the air, the cut chart, and the nest right in that order, and the CNC becomes the reliable part of the process instead of the thing you are constantly adjusting.